

This report details the proposed processing design for restarting the Copper Rand mill to treat blended mineralized material from three deposits, supported by historical operating data and testwork.
Report context
This June 2022 technical report (NI 43-101) presents a preliminary economic assessment (PEA) for the Chibougamau Hub-and-Spoke Complex, owned by Doré Copper Mining Corp. The report describes recovery methods for mineralized material from the Corner Bay, Delvin, and Joe Mann deposits, processed through the Copper Rand mill, which has been closed since 2008.
Processing route
Crushing and mineral sorting
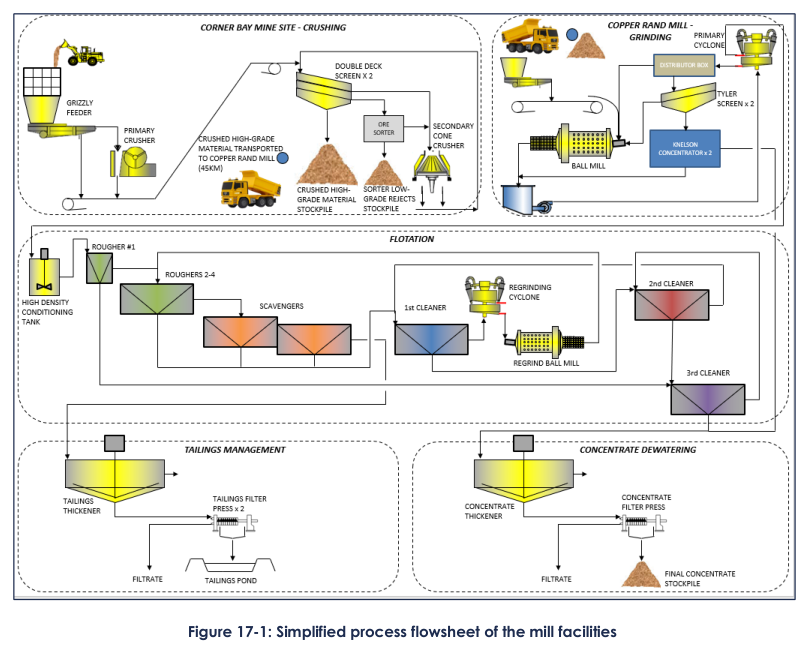
The crushing circuit is proposed for installation at the Corner Bay mine site. It comprises a grizzly feeder feeding a primary jaw crusher sized at 30 in × 42 in (76.2 cm × 106.7 cm) for a daily throughput of 3,600 t/d. The jaw crusher is rated with a connected power of 125 hp (93 kW). The crusher selection is based upon a feed size of 362 mm and a product P80 of 90 mm.
The jaw crusher product and grizzly undersize report to a single double-deck vibrating screen with a nominal feed size F80 of 64 mm. The top deck opening is 38 mm and the bottom deck opening is 10 mm. Top deck oversize is directed to the secondary cone crusher rated at 300 hp (224 kW). Bottom deck oversize reports to an integrated X-ray transmission (XRT) mineral sorter circuit. Screen undersize passes directly to the crushed material stockpile at the Copper Rand mill site.
The mineral sorter rejects low-grade and dilution material from the Devlin and Corner Bay mines. High-grade material is trucked to the Copper Rand mill site and stored in a covered stockpile under a mega-dome with approximately 50 hours of storage capacity.
Design crushing plant availability is 65%, operating for 5,690 hours per year. At full production, the crushing plant processes an average of 831.9 Kt/y of run-of-mine (ROM) material.
Grinding and gravity concentration
The grinding circuit is proposed for installation at the Copper Rand mill site. It consists of a single ball mill in closed circuit with classifying hydrocyclones. The ball mill has an installed power of 1,500 kW, reducing feed from 80% passing 8,148 µm to 1,064 µm, with a design feed of 2,240 t/d. The mill accommodates a design throughput of 2,240 t/d and a design feed rate of 93 t/h assuming a grind size of 80% passing 100 µm.
The ball mill product is sent to primary cyclones. The cyclone overflow, with a P80 of 100 µm, discharges to the flotation circuit. The underflow discharges to a distributor box, splitting into two streams: approximately two thirds of the slurry returns to the ball mill and approximately one third reports to two vibrating screens feeding two Knelson gravity concentrators operating in parallel. Gravity concentrate from the Knelson concentrators is sent directly to the final copper concentrate. Gravity tails are returned to the hydrocyclone feed pump box.
Design mill availability is 95%, operating for 8,322 hours per year. At full production, the mill processes an average of 492.8 Kt/y of mineralized material.
Flotation circuit
The ground product from the grinding circuit reports to a conditioning tank where chemical reagents are added. The conditioned material is floated to yield a copper concentrate.
The conditioning tank discharge is directed to the first rougher cell bank, comprised of one 32 m³ Maxwell 12 flotation cell. Concentrate from this cell reports directly to the third stage of cleaner flotation. Tailings report to three 20 m³ Maxwell 10 flotation cells operated in series. Nominal flotation time is 16 minutes at 42% solids density. Concentrate from these second rougher cells reports to the first stage of cleaner flotation with a target grade of 10% Cu. Second rougher tailings report to the scavenger flotation cells.
Scavenger flotation consists of six 14 m³ Denver DR-500 flotation cells. Scavenger concentrate is sent to the first stage of cleaner flotation. Scavenger tailings are collected and pumped to the tailings filtration circuit.
The first cleaning stage comprises four Denver DR-300 flotation cells, each with a capacity of 8.5 m³. First cleaner concentrate reports to the second cleaning stage. First cleaner tailings are collected and pumped to the regrind ball mill, then returned to the second stage of rougher flotation.
The second stage cleaner circuit consists of four Denver DR-300 flotation cells, each with a capacity of 8.5 m³. Tailings from the second stage are recirculated to the first cleaner.
The third stage cleaner circuit consists of four Denver DR-200 flotation cells, each with a capacity of 5.1 m³. Tailings from the third bank are recycled to the second cleaner circuit. Concentrate grade is expected to be 23.7% Cu.
The flotation circuit includes a regrind ball mill and a regrind hydrocyclone.
Concentrate and tailings dewatering
The final concentrate, a combination of product from the gravity circuit and the third cleaner, is directed to an 8 m diameter concentrate dewatering thickener equipped with an agitator, then passes through a filter press that recovers concentrate with a moisture content of 8%. Copper concentrate is sent to a concentrate stockpile for transport.
Total final tailings from the scavenger circuit, at 30% solids density, are thickened and filtered to reach approximately 88% solids. The filtration plant is located in a new building next to the mill and comprises two filter presses, both operating with no standby, each with 50 chambers (3.9 m³ per chamber). Filters bring the moisture content of the filter cake to 12%. Filtrate and wash water are collected and pumped back to the process. Filter cake is discharged onto a conveyor to a stockpile, then loaded onto trucks and transported to the dry stack tailings facility (TMF).
Plant modifications and ramp-up
Several modifications are proposed to the existing Copper Rand processing plant to accommodate treatment of three different mineralized material sources. These include decommissioning of the existing crushing and grinding sections; addition of a new crushing circuit at Corner Bay including a mineral sorter; addition of a new grinding circuit; addition of a conditioning tank; expanded capacity of the concentrate filter; addition of a new tailings filter plant; and reconfiguration of piping around the flotation circuit.
From Year 4 to Year 7, an increase in tonnage is expected with increased mined tonnes from Corner Bay and processing of Joe Mann material. At Year 3, additional capacity will be added at the rougher and cleaner flotation stages to accommodate this increase, including a new 50 m³ rougher tank cell and additional cells to the existing cleaner flotation banks.
Consumables and process water
Primary reagents include collector KAX51 (131 t/y), collector R208 (7 t/y), frother MIBC (25 t/y), hydrated lime (830 t/y), and flocculant (14 t/y). Grinding media consumption is 339 t/y of 50 mm diameter balls for the primary ball mill and 68 t/y of 25 mm diameter balls for the regrind ball mill. Consumption rates are mostly based upon historical operational data.
Process water is provided by recirculation from thickener overflows, surface water, or reclaim water. The process water system supplies the grinding, flotation, and dewatering circuits. Fresh water from surface sources or tailings pond reclaim supplies reagent preparation and equipment gland seals.
Concentrator personnel
A total of 72 employees are required in the process plant, comprising 12 salaried staff and 60 hourly workers. The crushing plant requires 10 hourly workers; the processing plant requires 50 hourly workers.
Electricity
Average power demand is estimated at 40.75 GWh for both the crushing and process plants, based on Hydro-Québec’s average cost of $0.0527/kWh.
Key reported parameters
| Parameter | Unit | Value |
|---|---|---|
| General design data | ||
| Process plant operating life | y | 11 |
| Crusher plant availability | % | 65 |
| Crusher operating hours per year | hr | 5,690 |
| Mill availability | % | 95 |
| Mill operating hours per year | hr | 8,322 |
| Crushing plant feed | ||
| Average yearly ROM feed | t/y | 831,883 |
| Design hourly feed tonnage | t/h | 220 |
| Average hourly feed tonnage | t/h | 146 |
| Average ROM grade | % Cu | 2.61 |
| Mill feed and production | ||
| Design mill feed | t/h | 93 |
| Average mill feed | t/h | 56 |
| Average yearly mill feed | t/y | 492,750 |
| Average mill feed grade | % Cu | 4.71 |
| Average concentrate production | t/y | 85,475 |
| Average concentrate grade | % Cu | 23.7 |
| Concentrate humidity | % H₂O | 8 |
| Copper recovery (Corner Bay) | ||
| Overall crushing and sorting copper recovery (A) | % | 96.4 |
| Gravity and flotation copper recovery (B) | % | 96.7 |
| Overall copper recovery (A × B) | % | 93.2 |
| Copper recovery (Devlin) | ||
| Overall crushing and sorting copper recovery (A) | % | 97.2 |
| Gravity and flotation copper recovery (B) | % | 98.2 |
| Overall copper recovery (A × B) | % | 95.5 |
| Copper recovery (Joe Mann) | ||
| Gravity and flotation copper recovery | % | 93.9 |
Project website: https://www.cygnusmetals.com/chibougamau-camp/
Note: The overall combined recovery of the mineral sorter and mill is stated as 93.3% copper in the report text. Table 17-1 reports overall recovery for Corner Bay at 93.2%, Devlin at 95.5%, and Joe Mann at 93.9% (gravity and flotation only; no sorting recovery is reported for Joe Mann).
Technical qualifications
The recovery methods described in this report were established on the basis of historical operational data and testwork as described in Section 13 of the report, equipment information from suppliers, and engineering experience on similar projects. The work forms the basis of the plant design, capital costs, and operating costs developed in this study. All sizing was made to accommodate the highest throughput from ROM with a design factor of 15%. Operating costs are based on average crusher and mill feed over the life of mine. The report presents a preliminary economic assessment and is not a feasibility study.
Source: Doré Copper Mining Corp., NI 43-101 Technical Report, PEA for the Chibougamau Hub-and-Spoke Complex, June 2022, Sections 1.16 and 17.
Consolidated report summaries
The following former standalone pages about this operation were consolidated here in October 2026. They are retained for source traceability; dates and figures reflect each report’s own effective date and may be superseded by the current information above.
Joe Mann Project — 2021 Technical Report
This 2021 technical report reviews historical processing of Joe Mann ore (2005–2007) at the Copper Rand Mill, a facility that has been idle since 2008 and would require component evaluation before any restart.
Report context
This profile is based on the NI 43-101 technical report for the Joe Mann Project, prepared by SLR Consulting (Canada) Ltd. for Doré Copper Mining Corp., with an effective date of July 21, 2021. The report describes a former gold–copper–silver mine in northwestern Québec that operated intermittently from the 1960s to 2007. No new metallurgical testing had been initiated by Doré Copper at the time of reporting. Between January 2005 and September 2007, Joe Mann ore was trucked approximately 60 km to the Copper Rand Mill, a facility that processed the ore on a toll or owner-operator basis. The Copper Rand Mill operated from 1959 until the end of 2008, when it was shut down and its process vessels emptied, with mills raised on jacks to protect bearings. The report explicitly states that the mill has not been operational since that time and that prior to any restart each component would require evaluation, repair, or replacement.
Processing route
The Copper Rand Mill flowsheet, as described in the 2021 report, comprises crushing, primary and secondary grinding with gravity gold recovery, flotation, concentrate regrind and cleaning, thickening, and filtration.
Crushing and fine ore storage
Three stages of crushing are employed: a 30 in. × 42 in. jaw crusher as the primary, followed by a 5½ ft standard cone crusher and a 5½ ft short head cone crusher as secondary and tertiary units. Both cone crushers operate in closed circuit with two double-deck vibrating screens (72 in. × 192 in.). Screen undersize is conveyed to three fine ore bins, each of 1,300 st capacity (approximately 1,179 t per bin), for mill feed storage.
Primary grinding and gravity circuit
Crushed ore is fed to a 9½ ft × 12 ft rod mill operating in open circuit. Rod mill discharge is pumped to a primary grinding circuit consisting of two 9 ft × 10 ft ball mills in closed circuit with primary hydrocyclone classifiers (18 in. cyclones) and two 30 in. primary Knelson concentrators. The overflow from the primary hydrocyclones reports to secondary hydrocyclones.
Secondary grinding and gravity circuit
Underflow from the secondary hydrocyclones feeds an 8 m³ flash flotation cell and a 30 in. secondary Knelson concentrator. Concentrate from both stages of Knelson gravity separation is directed to a 4 ft × 8 ft shaking table for final gold and silver concentrate production, which is then melted in a furnace. Flash flotation concentrate is sent directly to the concentrate thickener, while flash flotation tailings are pumped to the secondary ball mill grinding circuit. The secondary grinding stage uses two ball mills: one 8 ft × 12 ft (400 hp) and one 9½ ft × 12 ft (500 hp).
Flotation circuit
Feed to flotation comes from the overflow of the secondary hydrocyclones. The flotation circuit comprises:
- Four Maxwell rougher tanks (one 32 m³ and three 20 m³)
- Two Denver 500 scavenger banks
- Three Denver cleaner banks (200 ft³, 200 ft³, 300 ft³, and 500 ft³ units)
Rougher concentrate is sent to a 7 ft × 10 ft regrind ball mill and then cleaned through three stages of cleaner cells before being pumped to the concentrate thickener. Tailings or middlings from the cleaning circuit can be returned either to the first cleaner or to the rougher circuit. Scavenger concentrate is recycled to rougher flotation; scavenger tailings proceed to the tailings pond.
Thickening and filtration
Thickened concentrate from a 36 ft × 10 ft Dorr-Oliver thickener is pumped to a Lasta filter press (1500 × 28 × 22 mm), then washed, dried, discharged, and stored. An 8 ft × 6 ft disc filter is also listed in the circuit.
Key reported parameters
| Parameter | Value | Basis |
|---|---|---|
| Ore transport distance (Joe Mann to Copper Rand Mill) | ~60 km | Historical operation (2005–2007) |
| Crushing stages | Three-stage (jaw, standard cone, short head cone) | Installed equipment, idle since 2008 |
| Fine ore bin capacity (each) | 1,300 st (approx. 1,179 t) | Installed; three bins total |
| Rod mill | 9½ ft × 12 ft, 550 hp | Installed, open circuit |
| Primary ball mills (two) | 9 ft × 10 ft, 400 hp each | Installed, closed circuit with hydrocyclones |
| Primary Knelson concentrators (two) | 30 in., 15 hp each | Installed |
| Secondary ball mills (two) | 8 ft × 12 ft (400 hp) and 9½ ft × 12 ft (500 hp) | Installed |
| Secondary Knelson concentrator | 30 in., 15 hp | Installed |
| Flash flotation cell | 8 m³ | Installed |
| Rougher flotation cells (Maxwell) | One 32 m³ (10.5 hp); three 20 m³ (10 hp each) | Installed |
| Regrind ball mill | 7 ft × 10 ft, 200 hp | Installed |
| Cleaner flotation cells (Denver) | 200 ft³ (20 hp), 200 ft³ (20 hp), 300 ft³ (30 hp), 500 ft³ (40 hp) | Installed |
| Concentrate thickener (Dorr-Oliver) | 36 ft × 10 ft | Installed |
| Filter press (Lasta) | 1500 × 28 × 22 mm | Installed |
| Historical gold recovery (2005–2007) | Reported in Table 13-1 of source | Actual mill performance; values not extracted from OCR-ambiguous table |
| Historical copper recovery (2005–2007) | Reported in Table 13-1 of source | Actual mill performance; values not extracted from OCR-ambiguous table |
| Historical silver recovery (2005–2007) | Reported in Table 13-1 of source | Actual mill performance; values not extracted from OCR-ambiguous table |
Technical qualifications
This profile is a snapshot of the 2021 technical report. The Copper Rand Mill has been idle since 2008; all equipment described is installed but non-operational. The report explicitly states that prior to restart, each component must be evaluated and any repairs or replacements completed. No metallurgical testing had been initiated by Doré Copper for the Joe Mann project at the time of reporting. The historical recovery data (2005–2007) are presented in the report as a summary table but specific numerical values are not reproduced here due to OCR ambiguity in the source markdown. The report notes that information regarding the specific mineralized zones extracted from the Joe Mann deposit during that period is unknown. The flowsheet description and equipment list show the configuration at the time of the mill’s closure; no design or proposed modifications are presented in the cited sections.
Source: Technical Report on the Joe Mann Project, Northwest Québec, Canada, prepared for Doré Copper Mining Corp. by SLR Consulting (Canada) Ltd. (SLR Project No: 233.03410.R0000). Effective date July 21, 2021; signature date September 10, 2021. Sections 13.0 (Mineral Processing and Metallurgical Testing) and 17.0 (Recovery Methods).
Corner Bay-Devlin Property — 2021 Technical Report
Corner Bay-Devlin Property — 2021 Technical Report
| Company | Doré Copper Mining Corp. |
| Date | 2021-11-10 |
| Region | Chibougamau, Quebec, Canada |
| Commodities | Gold, Silver, Copper |
| Status | Development |
Executive Summary
This section of the NI 43-101 Technical Report outlines the proposed recovery methods for the Corner Bay-Devlin Property, owned by Doré Copper Mining Corp. The plan involves treating mineralized material from the Corner Bay and Devlin deposits at the existing Copper Rand Mill, located approximately eight kilometers southeast of Chibougamau. The mill has been non-operational since the end of 2008, and a comprehensive evaluation and repair program is required before a restart can occur.
The proposed process flow sheet details a multi-stage crushing circuit followed by grinding, gravity concentration, and flotation. The crushing circuit utilizes a jaw crusher as the primary unit, supported by standard and short head cone crushers in a closed circuit with vibrating screens. The crushed ore is then processed through a rod mill and ball mill circuit, incorporating primary and secondary Knelson concentrators for gravity recovery of gold and silver.
The flotation circuit employs Maxwell rougher tanks and Denver scavenger and cleaner banks to recover additional valuable minerals. The final concentrates are thickened, filtered using a filter press and disc filter, and stored. The report provides detailed equipment specifications and flow sheet descriptions, emphasizing the need for component evaluation and potential replacements to ensure the mill can be successfully restarted for production.
Website: https://www.juniorminingnetwork.com/junior-miner-news/press-releases/2751-tsx-venture/cyg/163619-dore-copper-enters-into-an-agreement-to-acquire-claims-next-to-its-flagship-corner-bay-high-grade-copper-deposit.html
Report Date: 2021-11-10
Region: Chibougamau, Quebec, Canada
Project Status: Development
Commodity: Gold, Silver, Copper
Throughput:
Mine Life:
Mine Type:
Ore type:
