

Generation Mining's March 2025 feasibility study update for the Marathon copper-palladium project in northwestern Ontario ramps up to 27,700 t/d in Year 3 and adds a pebble crusher and tailings thickener at that stage.
The Marathon Copper-Palladium Project Feasibility Study Report Update, Marathon, Ontario, was prepared by Ausenco Engineering Canada and others for Generation Mining Limited, with an effective date of November 1, 2024 and a report date of March 28, 2025. The plant design rests on feasibility-study metallurgical testwork and the economic analysis that followed. The plant starts at 25.2 kt/d (9.2 Mt a year) and ramps up to 27.7 kt/d (10.1 Mt a year) in Year 3. The life-of-mine feed grade averages 0.21% copper and 0.63 g/t palladium.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Report effective date | November 1, 2024 | Not applicable | Ausenco for Generation Mining Limited |
| Throughput | 9.2 Mt/a initially, 10.1 Mt/a from Year 3 | Not applicable | 25.2 and 27.7 kt/d |
| Life-of-mine grade | 0.21% Cu, 0.64 g/t Pd, 0.20 g/t Pt, 0.07 g/t Au, 1.67 g/t Ag | Not applicable | Design criteria table |
| Availability | 72.3 crushing, 90.7 grinding and flotation, 83.2 filtration | % | Two 12-hour shifts, 365 days |
| Primary crusher | Gyratory, 1,915 t/h | Not applicable | Crushes ore and waste |
| SAG mill | 10.36 x 6.10 m, 16.25 MW twin pinion | Not applicable | Pebble crusher added after ramp-up |
| Ball mill | 8.08 x 12.34 m, 16.25 MW twin pinion | Not applicable | 400% circulating load |
| Flotation feed | k80 106 | µm | 35% solids |
| Rougher flotation | Five 630 m³ tank cells, 60 min | Not applicable | PAX, Aero 3501, MIBC |
| Regrind | 2,500 kW HIG mill to k80 18 µm | Not applicable | Ceramic media; 30 min aeration |
| Cleaners | Three stages of SFR cells | Not applicable | Staged flotation reactors |
| Concentrate moisture | Below 12 | % | Thickening and filtration |
Overview
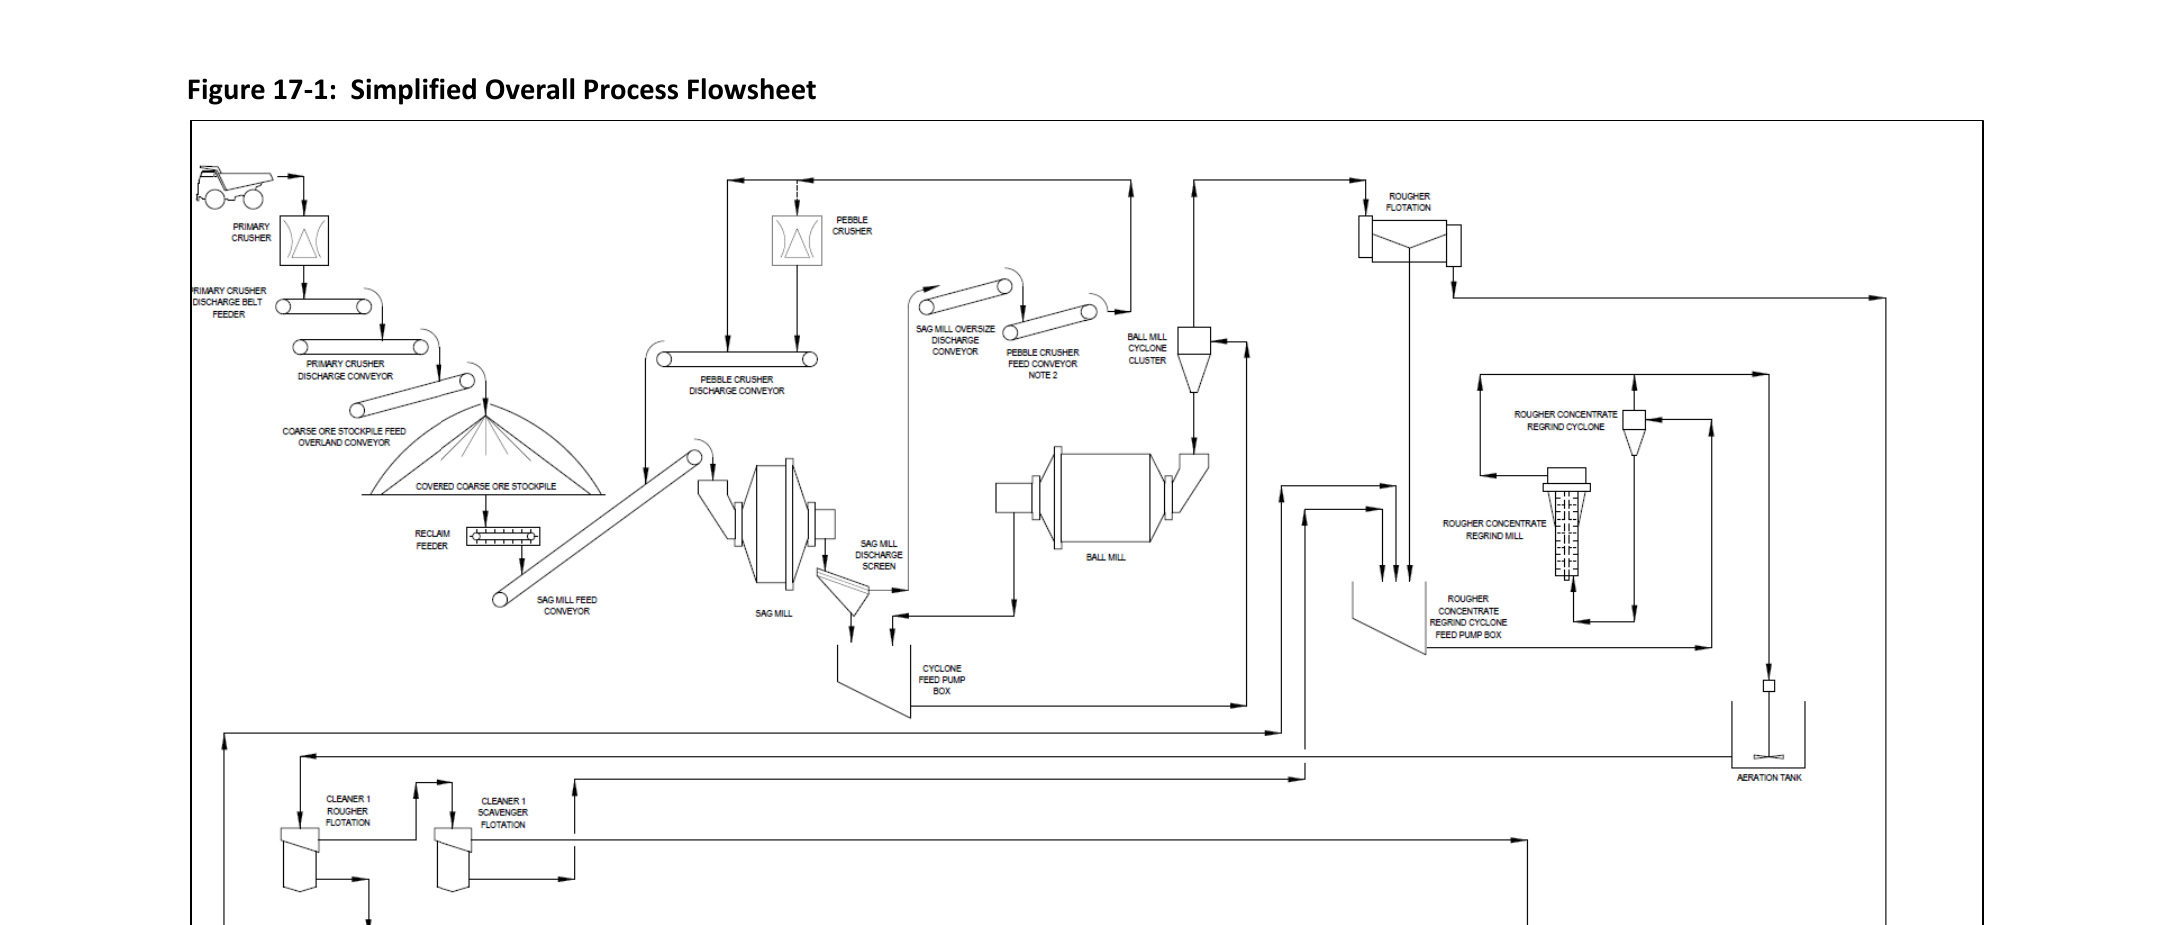
The plant has four main areas: crushing and grinding, flotation and regrind, concentrate thickening and filtration, and tailings thickening. Run-of-mine ore is crushed in a primary gyratory crusher and conveyed to a stockpile, then ground in a SAG mill and ball mill closed with cyclones. Rougher flotation is followed by regrinding and aeration of the rougher concentrate and three stages of cleaning in staged flotation reactor (SFR) cells. The final copper-PGM concentrate is thickened and filtered to below 12% moisture. Testwork from 2020 to 2022 showed that regrinding and aerating the rougher concentrate are needed for better liberation and to maximize concentrate grade.
Key Process Stages
Primary crushing. 240 t haul trucks tip into a 396 t dump pocket over the gyratory crusher, which crushes both ore and waste at 1,915 t/h. A diverter chute sends ore to the coarse ore stockpile and crushed waste, about 2.0 Mt a year for tailings dam and site construction, to a 3,792 t waste stockpile. A metal detector and magnet remove tramp metal, and a mobile breaker handles rocks over the 1,000 mm top size.
Stockpile and reclaim. The coarse ore stockpile holds 15,288 t live, 12 hours of mill feed. Two apron feeders (duty and standby) deliver 1,274 t/h to the SAG feed conveyor.
Grinding. The SAG mill runs at 75% solids. In the initial phase its discharge passes a single-deck screen, and pebbles are returned to the mill. After ramp-up, a pebble crusher crushes them first. The ball mill is closed with a cluster of 14 cyclones of 650 mm (11 operating), producing a k80 of 106 µm. PAX and Aero 3501 are added at the cyclone feed, and an on-stream analyzer measures copper and PGM in the cyclone overflow.
Rougher flotation. Five 630 m³ tank cells in series give 60 minutes of residence, with PAX (45 g/t), Aero 3501 (22.5 g/t) and MIBC (23 g/t). Rougher tails are thickened (from Year 3) and sent to the tailings storage facility (TSF).
Regrind and aeration. Rougher concentrate, first cleaner scavenger concentrate and second cleaner tails are classified in open-circuit cyclones that pass fines below 18 µm. The underflow, at 40 to 45% solids, is ground in a 2,500 kW HIG mill with ceramic media to k80 18 µm. Both streams then pass a 30-minute pre-aeration tank.
Cleaning. Seven first cleaner, three first cleaner scavenger, five second cleaner and five third cleaner SFR cells produce the final concentrate. First cleaner scavenger tails are pumped to a segregated tailings area.
Additional Interesting Data and Summary
Services include lime slaking, flotation reagents, water treatment, flocculant, compressed air for the SFR cells, and air blowers for the conventional cells. Steel balls are added by kibble and crane, and an additional liner handler is planned to share mill maintenance.
In summary, the 2025 Marathon feasibility update is a conventional SAG-ball and flotation plant for a low-grade copper-palladium deposit at about 25,000 to 28,000 t/d. It relies on fine HIG regrinding to 18 µm, pre-aeration and SFR cleaner cells to make a saleable copper-PGM concentrate.
Key Processes
- Gyratory crushing of ore and construction waste
- SAG milling (pebble crushing after ramp-up) and ball milling to k80 106 µm
- Rougher flotation in 630 m³ tank cells
- HIG regrind of rougher concentrate to k80 18 µm
- Pre-aeration of reground concentrate
- Three-stage SFR cleaner flotation
- Concentrate thickening and filtration
- Rougher tailings thickening and segregated cleaner tailings disposal
Source: Marathon Copper-Palladium Project Feasibility Study Report Update, Marathon, Ontario, Canada, prepared by Ausenco Engineering Canada ULC for Generation Mining Limited, effective date November 1, 2024.
Consolidated report summaries
The following former standalone pages about this operation were consolidated here on October 25, 2026. They are retained for source traceability; dates and figures reflect each report’s own effective date and may be superseded by the current information above.
Marathon Property — 2019 Pre-Feasibility Study
Metallurgical testwork and flowsheet design for the Marathon Project support a split copper-PGM flotation circuit with fine grinding and multiple cleaning stages, processing 5 Mtpa in years 1–5 and expanding to 8 Mtpa from year 6 onward.
Report context
The Marathon Property Pre-Feasibility Study (PEA) technical report was prepared by P&E Mining Consultants Inc. for Generation Mining Limited and is dated 2019. The report presents a process plant design based on extensive bench-scale metallurgical testing conducted over several years at multiple laboratories, including crushing, grinding, batch, cycle, and mini pilot-scale froth flotation testing. The most recent tests focused on confirming circuit stability, maximizing concentrate grade, and representing a split Cu-PGM flowsheet with fine grinding and multiple cleaning stages in each flotation circuit.
Processing route
Primary crushing and stockpiling
Run-of-mine mineralized material is hauled by 221 t haul trucks from the open pit and dumped directly into a gyratory primary crusher (Metso 54/75 inch, 450 kW installed power) that reduces material from less than 1,000 mm to a product size of P80 150 mm. The crusher has an operating capacity of 1,750 tph and is scheduled to operate 8.5 hours per operating day to process 5 Mtpa. Crushed material drops into a surge bin, onto an apron feeder, and is transported by a 100 m conveyor to a covered stockpile. The stockpile is contained under a permanent unheated conical dome to prevent snow and rain intrusion and has a capacity of approximately 100,000 tons (about 7 days).
Grinding circuit (Phase 1)
Stockpiled material is reclaimed by four apron feeders (in two pairs) and conveyed to a SAG mill. The SAG mill is nominally 9.7 m diameter by 4.3 m long with 7,460 kW installed power, oversized for 5 Mtpa but suitable for 8 Mtpa. The SAG mill discharges over a vibrating screen with 76 mm openings; oversize pebbles are returned to the SAG feed after crushing in a short head cone crusher (2.3 m × 2.5 m × 2.6 m, 315 kW) to 15 mm. Undersize feeds a ball mill (6.7 m diameter by 9.1 m long, 7,460 kW) operating in closed circuit with cyclones at a circulating load of up to 250%. Cyclone overflow targets P80 of 200 µm (212 µm per design criteria) and flows to copper rougher flotation.
Copper flotation circuit
The copper rougher circuit comprises two rows of four 50 m³ Outotec e50 flotation cells (eight cells total in Phase 1) with 20 minutes residence time. Reagents include potassium amyl xanthate (PAX) and MIBC frother, with milk-of-lime slurry added for pH control. Copper rougher concentrate is re-ground in a VertiMill (Metso VTM-800-EB) to P80 of 20 µm in closed circuit with cyclones. Re-ground concentrate feeds a 4-stage cleaner circuit: three 10 m³ Outotec e10 first cleaner cells, two 10 m³ e10 cleaner-scavenger cells, four 4 m³ Metso DR24 second cleaner cells, and two 10 m³ column cells in series for third and fourth cleaning. Copper cleaner-scavenger tailings are sent to the PGM re-grind circuit.
PGM flotation circuit
Copper rougher tailings are re-ground in a ball mill (6.7 m diameter by 9.1 m long, 7,460 kW) in closed circuit with cyclones to produce a PGM rougher feed of P80 100 µm. PGM rougher flotation uses two banks of four 50 m³ Outotec e50 cells (eight cells total in Phase 1) with 20 minutes residence time. PGM rougher concentrate is re-ground to P80 of 10 µm using either two VertiMills (one operating, one standby) or a horizontal stirred mill such as an IsaMill with ceramic grinding media. The ground concentrate undergoes four stages of cleaning: 20 minutes residence time in three 10 m³ Outotec e10 first cleaner cells, followed by three 10 m³ e10 first cleaner-scavenger cells, four 4 m³ Metso DR24 second cleaner cells, and two column cells (0.45 m diameter by 10 m high, 10 m³ each) for third and fourth cleaning.
Concentrate handling
Copper and PGM concentrates are combined in a concentrate thickener (14 m diameter) where feed slurry is mixed with flocculant and thickened to 60% solids. Thickened concentrate is pumped to plate and frame pressure filters, reducing moisture to 10% or less (target 8%). If moisture exceeds 10%, a Holoflite-type dryer may be considered. Concentrate can be shipped in bulk during mild weather; for winter shipment, heated containers or bagging in 1-tonne lots is proposed.
Residual sulphide flotation
PGM rougher tailings feed a conditioner tank (over 10 minutes retention) where depressed sulphides are reactivated by pH adjustment and/or carbon dioxide addition. Up to five 50 m³ flotation cells produce a moderately enriched sulphide concentrate that becomes Type 2 process solids (potentially acid generating). Sulphide flotation tailings become Type 1 process solids (non-acid generating). Both streams are thickened to approximately 50% solids before separate pumping to the process solids management facility.
Phase 2 expansion (year 6 onward)
From production year 6 to end of life-of-mine, the process plant treats 8 Mtpa. Expansion includes: primary crusher operation increasing from 8.5 to 13.5 hours per day; addition of a secondary cone crusher (Metso HP800 or equivalent) with a screen deck for 75 mm material; installation of a second ball mill; and additional flotation cells (10 Outotec e50 rougher cells for copper, 10 for PGM; larger cleaner circuits). Ramp-up to 8 Mtpa is estimated at 85% in Q1 of year 6, then 100% thereafter.
Key reported parameters
| Parameter | Unit | Phase 1 (Years 1–5) | Phase 2 (Years 6+) | Basis |
|---|---|---|---|---|
| Nominal annual input | dry tpa | 5,000,000 | 8,000,000 | Design |
| Operating days per year | days | 350 | 350 | Design |
| Nominal daily input | dry tpd | 14,300 | 22,900 | Design |
| Primary crusher type | , | Metso 54/75" gyratory | Metso 54/75" gyratory | Design |
| Primary crusher installed power | kW | 450 | 450 | Design |
| Primary crusher feed F80 | mm | 500 | 500 | Design |
| Primary crusher closed side setting | mm | 150 | 150 | Design |
| Secondary crusher | , | , | Metso HP800 | Design |
| SAG mill dimensions (dia. × EGL) | m | 9.7 × 4.3 | 9.7 × 4.3 | Design |
| SAG mill installed power | kW | 7,460 | 7,460 | Design |
| SAG mill product P80 | mm | 2.5 | 2.5 | Design |
| Ball mill dimensions (dia. × EGL) | m | 6.7 × 9.1 | , | Design |
| Ball mills – number | No. | 1 | 2 | Design |
| Ball mill installed power | kW | 7,460 | TBD | Design |
| Primary grinding P80 | µm | 200 | , | Design |
| Copper rougher residence time | min | 20 | 20 | Design |
| Copper rougher cell volume | m³/cell | 50 | 50 | Design |
| Copper rougher cells (2 lines) | No. | 8 | 10 | Design |
| Copper rougher conc. regrind P80 | µm | 20 | 20 | Design |
| PGM rougher residence time | min | 20 | 20 | Design |
| PGM rougher cell volume | m³/cell | 50 | 50 | Design |
| PGM rougher cells (2 lines) | No. | 8 | 10 | Design |
| PGM rougher conc. regrind P80 | µm | 10 | 10 | Design |
| Concentrate thickener diameter | m | 14 | 14 | Design |
| Concentrate filter cake moisture | % | 10 | 10 | Design |
| Abrasion Index (AI) | kWh/t | 0.396 | 0.4 | Micon (2008) |
| Bond Ball Mill Work Index | kWh/t | 16 | 16 | Micon (2008) |
| Copper recovery (years 1–5) | % | 92 | , | Testwork-based PEA estimate |
| Copper recovery (years 6+) | % | , | 90 | Testwork-based PEA estimate |
| Palladium recovery | % | 82.9 | 82.9 | Testwork-based PEA estimate |
| Platinum recovery | % | 74.5 | 74.5 | Testwork-based PEA estimate |
| Gold recovery | % | 73.2 | 73.2 | Testwork-based PEA estimate |
| Silver recovery | % | 71.5 | 71.5 | Testwork-based PEA estimate |
Project website: https://genmining.com/news/2025/generation-mining-expands-its-land-package-at-the-marathon-district/
Technical qualifications
The process plant recoveries for this PEA were determined by P&E to be as stated above, based on metallurgical testwork. The flowsheet design and equipment selection are derived from bench-scale testing and preliminary engineering; all major equipment items are subject to detailed review and adjustment following advanced engineering studies. The PGM circuit detailed design (e.g. for a Feasibility Study) requires consideration of opportunities for economic expansion to 8 Mtpa, including scheduled changes in feed grade, scale-up of flotation, grinding, pumping, and thickening capacities, supplemented by metallurgical performance experience during the first years. Fine grinding methodology and grinding media type require additional testwork. The use of reclaim water is assumed not to adversely affect flotation performance, with minor treatment or fresh-water addition as contingency. The report notes that HPGR technology was considered by previous studies but was not selected for this PEA; P&E suggests that a conventional SAG-ball mill combination presents lower risk for northern Canadian operations.
*Source: Marathon Property, 2019 Pre-Feasibility Study, Generation Mining Limited, P&E Mining Consultants Inc. Report No. 367, Sections 1.14, 1.15, 17.1–17.16.*
Marathon Palladium & Copper Project — 2021 Feasibility Study (Section 17)
Section 17 of the March 2021 feasibility study describes the proposed process plant design to produce a copper-PGM flotation concentrate from the Marathon Palladium & Copper Project in Ontario, Canada.
Report context
This feasibility study (FS) dated March 2021 presents the process design for the Marathon Palladium & Copper Project. The process plant is designed to process 25,200 t/d (9.2 Mt/y) at average life-of-mine feed grades of 0.21% copper and 0.63 g/t palladium to produce a copper-PGM flotation concentrate. The plant operating schedule is based on two 12-hour shifts per day for 365 days per year, with 70% availability for the crushing circuit, 92% for grinding and flotation circuits, and 85% for the concentrate filter.
Processing route
Primary crushing
Run-of-mine ore will be delivered to a primary gyratory crusher dump pocket by 216-t haul trucks or by front-end loader. The dump pocket has a capacity of approximately 580 t with dual side dumping. A hydraulically operated rock breaker will fracture oversize material. Crushed ore is withdrawn by a variable speed apron feeder and transferred to the primary crusher discharge conveyor, then to a 1.4 km overland conveyor feeding the coarse ore stockpile. A metal detector and magnet are located on the discharge conveyor for tramp metal protection.
Coarse ore stockpile and reclaim
Coarse ore feeds a single conical covered stockpile with total storage capacity of approximately 75,000 t. Nominal live capacity is 27% of total tonnes (18 hours retention). Remaining capacity can be recovered using a bulldozer or excavator. Two belt feeders, each capable of design throughput, transfer material to the SAG mill feed conveyor.
Grinding and pebble crushing
The grinding circuit consists of a single SAG mill (10.36 m diameter x 5.79 m effective grinding length, 15 MW twin pinion drives) followed by a single ball mill (7.92 m diameter x 11.28 m effective grinding length, 15 MW twin pinion drives) operating in closed circuit with a primary cyclopak. The SAG mill operates in closed circuit with a double deck screen and a pebble crusher. Screen undersize flows to the cyclone feed pump box. Pebble crusher discharge is recycled to the SAG mill feed conveyor. Primary cyclone overflow is the flotation feed with a target 80% passing size of 106 microns.
Rougher flotation and cleaner circuit
Primary cyclone overflow reports to the rougher flotation head tank. The rougher bank consists of ten direct flotation reactor cells. Rougher concentrate undergoes regrinding in two parallel HIG mills (5,500 kW each) to a target P80 of 18 μm. Reground concentrate reports to an iron sulfide aeration tank (30 minutes residence time) for pyrrhotite suppression at pH 11 prior to cleaning.
The cleaner circuit comprises three stages of flotation using DFR cells. First cleaner has six cells, second cleaner has six cells, and third cleaner has five cells. Cleaner scavenger flotation with four cells treats first cleaner tailings, with scavenger concentrate recycled to the rougher concentrate regrind circuit. Third cleaner concentrate is the final Cu-PGM concentrate.
Tailings coarse regrind and PGM scavenger flotation
Rougher tailings are classified by sand/slime cyclones. The coarse fraction (P80 +53 μm) is reground in two open-circuit HIG mills (5,500 kW each) to a product P80 of 38 μm. Reground material reports to PGM scavenger flotation comprising five DFR cells. PGM scavenger concentrate returns to the rougher concentrate regrind circuit. The fine fraction combines with PGM scavenger tailings as low-sulfide, non-PAG tailings directed to the tailings thickener.
Concentrate thickening and filtration
Final concentrate from the third cleaner is thickened in a single high-rate thickener (unit area thickening rate 0.28 m²/t/d) to 55-60% w/w solids underflow. Thickened concentrate is pumped to an agitated filter feed tank with 12 hours surge capacity, then to a single Outotec Larox PF 60/72 horizontal pressure filter producing cake at 10-13% w/w moisture. Filtrate returns to the concentrate thickener.
Concentrate storage and load out
Filter cake discharges by gravity to a concrete storage bunker with capacity for up to 7 days at nominal production rates. Concentrate is loaded by front-end loader into a chute feeding a belt conveyor for truck loading. Transport trucks are weighed on a load-out scale at site.
Tailings thickening and storage
Combined rougher tailings fine fraction and PGM scavenger tailings are thickened in a single 65 m diameter high-rate thickener (unit area thickening rate 0.12 m²/t/d) to 55-60% w/w solids. First cleaner scavenger tailings are pumped separately to designated sub-aerial locations within the tailings storage facility to mitigate oxidation and acid generation. Thickener underflow reports to the TSF by gravity or centrifugal pumping.
Reagents
Potassium amyl xanthate (PAX) is used as collector in rougher and cleaner flotation, delivered as pellets in bulk bags and mixed to 15% w/w solution. Cytec Aero 3501 acts as PGM collector, delivered as liquid in totes. Methyl isobutyl carbinol (MIBC) provides froth, delivered as liquid in totes. Carboxymethyl cellulose (CMC) is used as depressant in the cleaner circuit to improve final concentrate grades by depressing talc. Two flocculant mixing systems serve the concentrate and tailings thickeners. Quicklime is delivered in 30 t trucks for slaking, with lime slurry used primarily in the concentrate regrind circuit.
Water systems
Fresh water is supplied from the Water Management Pond or Storm Water Management Pond. Process water is sourced from tailings thickener overflow, concentrate thickener overflow, concentrate filtrate, return water from the TSF, and fresh water make-up. A dedicated firewater reserve of 400 m³ is contained in the fresh water tank.
Key reported parameters
| Description | Units | Value |
|---|---|---|
| Plant Capacity | Mt/y | 9.2 |
| LOM Average Feed Grade, Cu | % | 0.21 |
| LOM Average Feed Grade, Au | g/t | 0.07 |
| LOM Average Feed Grade, Ag | g/t | 1.42 |
| LOM Average Feed Grade, Pt | g/t | 0.20 |
| LOM Average Feed Grade, Pd | g/t | 0.63 |
| Crusher Operating Availability | % | 70.0 |
| Grinding and Flotation Operating Availability | % | 92.0 |
| Overall Concentrator and Filtration Systems | % | 84.6 |
| Stockpile Retention Time | hours | 18 |
| Ore Specific Gravity | – | 3.09 |
| SPI Value | min | 100 |
| Bond Crushing Work Index (CWi) | kWh/t | 18.6 |
| Bond Ball Work Index (BBWi) (75th percentile) | kWh/t | 16.5 |
| Primary Crusher Feed Size, F80 | mm | 425 |
| Primary Crushing Product, P80 | mm | 274 |
| Grinding Circuit Product Size, P80 | μm | 106 |
| SAG Mill Installed Power | MW | 15 |
| Ball Mill Installed Power | MW | 15 |
| Rougher Concentrate Regrind Specific Energy | kWh/t | 34 |
| Rougher Concentrate Regrind Product Size, P80 | μm | 18 |
| Coarse Tailings Regrind Specific Energy | kWh/t | 12.3 |
| Coarse Tailings Regrind Product Size, P80 | μm | 38 |
| Concentrate Filter Cake Moisture | % | 13 |
| Magnetic Concentrate Filter Cake Moisture | % | 9 |
| Pd Recovery Equation | % | 88.27 x (Pd head grade [Exp(0.0338)]) to max 92% |
| Pt Recovery Equation | % | 1.22 x (% Rec Pd) – 21.79 |
| Au Recovery Equation | % | 1.39 x (% Rec Pd) – 48.37 |
| Cu Recovery | % | 93.0 (constant) |
| Ag Recovery | % | 71.5 (constant) |
Project website: https://genmining.com/projects/overview/
Technical qualifications
The process design is based on information and metallurgical test results summarized in Section 13 of the report. Bench scale testing completed during 2020 applied conventional flotation cell technology. The evaluation of Woodgrove DFR cells during 2020 Phase 1 and Phase 2 metallurgical test programs supports a 20% decrease in baseline mass pull in the rougher and cleaner circuits relative to conventional flotation technology, with no change in metal recovery. Process mass balances for the FS applied the higher baseline mass pull for equipment sizing. Initial design concepts for the FS have excluded Cu-PGM concentrate magnetic separation. Determination of predictive recovery curves was established with the 2020 metallurgical testing programs, with estimated metal recovery defined in equations for the GeoMet model including the PGM-scavenger flotation circuit.
Source: Marathon Palladium & Copper Project Feasibility Study, March 2021, Section 17: Recovery Methods.
