

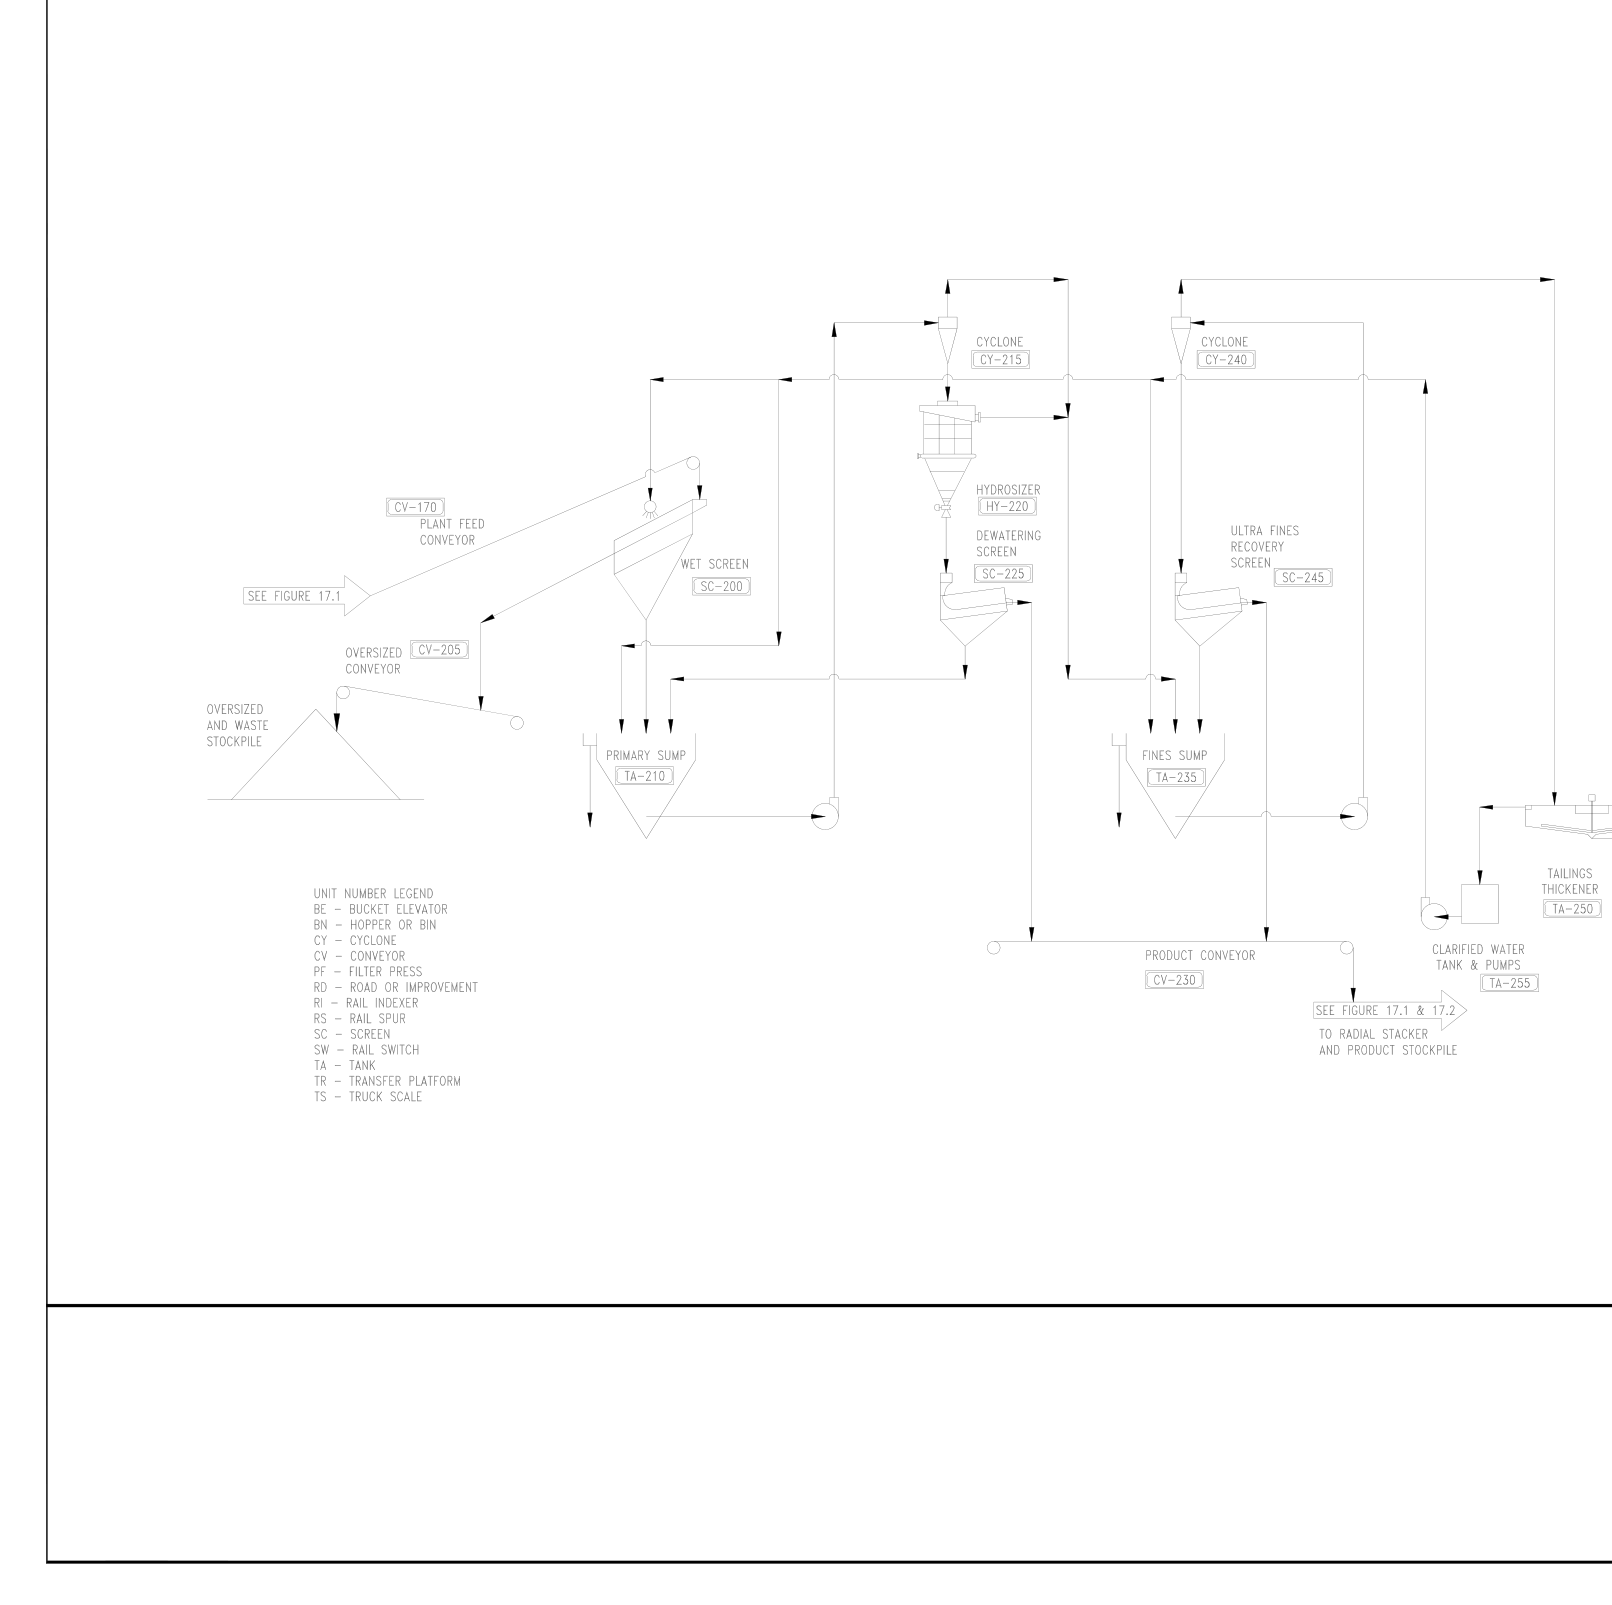
Athabasca Minerals' March 2015 preliminary economic assessment for the Firebag River Sand Property in Alberta pairs a rail transloading yard at Lynton with a wet plant, fluid bed dryers and a three-product dry plant at Edson.
The Firebag River Sand Property lies about 95 km north of Fort McMurray in northern Alberta. Athabasca Minerals Incorporated (AMI) commissioned Norwest Corporation to prepare a Preliminary Economic Assessment (PEA) of the sand property, with a report date of March 3, 2015 and an effective date of November 26, 2014. The study plans to mine 990,000 t/y of run-of-mine (ROM) sand, haul it by side dump truck to a rail loading site at Lynton, and move it by Canadian National (CN) trains to a processing plant at Edson. The sand is aimed at three potential frac sand sizes, 20/40 mesh, 40/70 mesh and 70/140 mesh. No processing happens at Lynton. All washing, drying and sizing happens at Edson.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| ROM mine production | 990,000 | t/y | Design basis |
| Annual scheduled hours | 5,500 | h | Not applicable |
| Plant availability | 90 | % | Not applicable |
| Annual operating hours | 5,000 | h | Not applicable |
| Plant feed rate | 175 | t/h | Wet plant nominal |
| Wet plant maximum | 200 | t/h | With a 5% finer feed |
| Rail loading capacity | 200 | t/h | Lynton |
| Train size | 100 | cars | Three independent sets of cars |
| Rail track at Lynton | About 6,000 | m | Plus main-line and yard switches |
| Rail transit cycle | 66 / 96 | h | Lynton to Edson / return |
| Thickener diameter | 15.2 | m | Ultra-fines |
| Slime and off-spec coarse | 20 to 25 | t/h | Preliminary sizing |
| Product sizes | 3 | grades | 20/40, 40/70 and 70/140 mesh |
Overview
The system is built around transport as much as processing. Sand is excavated at the property, trucked to Lynton, stockpiled and loaded on to trains. At Edson, a belly dump unloads the train and a radial stacker builds a ROM stockpile. A wet plant removes oversize and ultra-fines using screens, a cyclone, a hydrosizer and a thickener, and the washed sand drains in a product stockpile. A dry plant then dries the sand in two thermal dryers and splits it into three sizes on four mineral separators before storage, truck loading and dispatch.
Key Process Stages
Lynton rail loading
Side dump trucks unload excavated sand near a 75 t hopper filled from the ROM stockpile by a front-end loader. A train loading conveyor, rated at 200 t/h for the PEA, feeds bifurcated chutework that loads cars on either of two spurs. A car indexer positions the cars and a hydraulic ram pulls the full string of 100 cars along the spur, one car length at a time. CN drops off a set of 100 loaded cars and returns to Edson with 100 empties. With a 66 hour transit to Edson and 96 hours back, the system needs three independent sets of rail cars. Loading is planned year round, 24 hours a day, seven days a week. A release agent added at Lynton lets the sand release from the cars on arrival.
Edson unloading and stockpiling
The loaded train is switched onto a siding long enough to hold 100 cars and three locomotives off the main line, so other traffic can pass. Cars are trammed over a belly dump hopper, and three parallel drawdown feeders move sand to a transfer conveyor at 2,500 t/h. A radial stacker builds the ROM stockpile. Only the feeders, conveyor and stacker are sized up for quick unloading, with a target of less than four hours per train, not counting positioning. A front-end loader then feeds the plant hopper, and a vibratory pan feeder sets the 175 t/h feed rate.
Wet plant
The wet plant is a module-based design using screen classification and upward current separators (hydrosizers), with a cyclone ultra-fines system at the end. It has no attritioning or scrubbing step, since clay-bound fines are not expected in the mined seams. An 8 x 20 single-deck wet screen rejects plus 20 mesh as waste. Underflow reports to a primary sump, and a hydrocyclone and hydrosizer then make the initial split. The cyclone sits ahead of the hydrosizer to cut the fines load and give a sharper separation. The hydrosizer works with a countercurrent flow of teeter water that lifts ultra-fines away from the coarse sand. A high-frequency dewatering screen sends the hydrosizer product to the product conveyor. Ultra-fines pass to a second set of cyclones above a second high-frequency screen, and the cyclone overflow goes to a 15.2 m thickener. Thickener underflow is pumped to a plate and frame press instead of a settling pond, and the slime goes to an on-site reject area. The plant is housed in a prefabricated building on a floating-mat foundation, and the report recommends soil and bedrock work in future studies.
Dry plant
The washed sand free drains in a product stockpile and is then loaded into the dryer feed hopper. Two Ventilex fluid bed dryers use a control and feedback loop to modulate temperature and fuel use so the sand is not over dried. Dried sand goes by bucket elevator to polishing screens, and a set of splitters feeds four Rotex minerals separators that cut 20/40, 40/70 and 70/140 mesh products. Each product goes to its own bin, and a dual bin arrangement gives a buffer ahead of loading. The section from dryer to screens is enclosed, with a separate building for each product, and the dry plant and loadout have separate dust collection and ventilation systems.
Product dispatch
Highway haul trucks are weighed before and after loading, and a batching and dispatch system issues each truck a ticket that records tare weight and allowable gross vehicle weight.
Additional Interesting Data and Summary
The expected ROM size distribution is fine. Cumulative retained weight is 1.2% on 20 mesh and 22.9% on 45 mesh, reaching about 50.8% on 60 mesh, 83.3% on 100 mesh and 99.0% on 200 mesh, with 0.9% in the pan. That distribution is what the report uses for its conceptual design.
The report also lays out a project schedule that runs from a scoping study and environmental baseline work in 2014, through permits, detailed engineering and approvals, to earthworks, rail siding, a wet plant and a dry plant at Edson. It lists a natural gas tie-in as an allowance, and recommends that future studies characterize the reject stream.
Key Processes
- Truck haulage and rail transloading at Lynton
- Rail unloading and radial stacking at Edson
- Wet screening and hydrocyclone classification
- Hydrosizer removal of ultra-fines
- Thickening and plate and frame filtration of fines
- Fluid bed drying
- Dry screening into three product sizes
Source: Preliminary Economic Assessment, Firebag River Sand Property, March 3, 2015.
