Mineral Processing Circuit

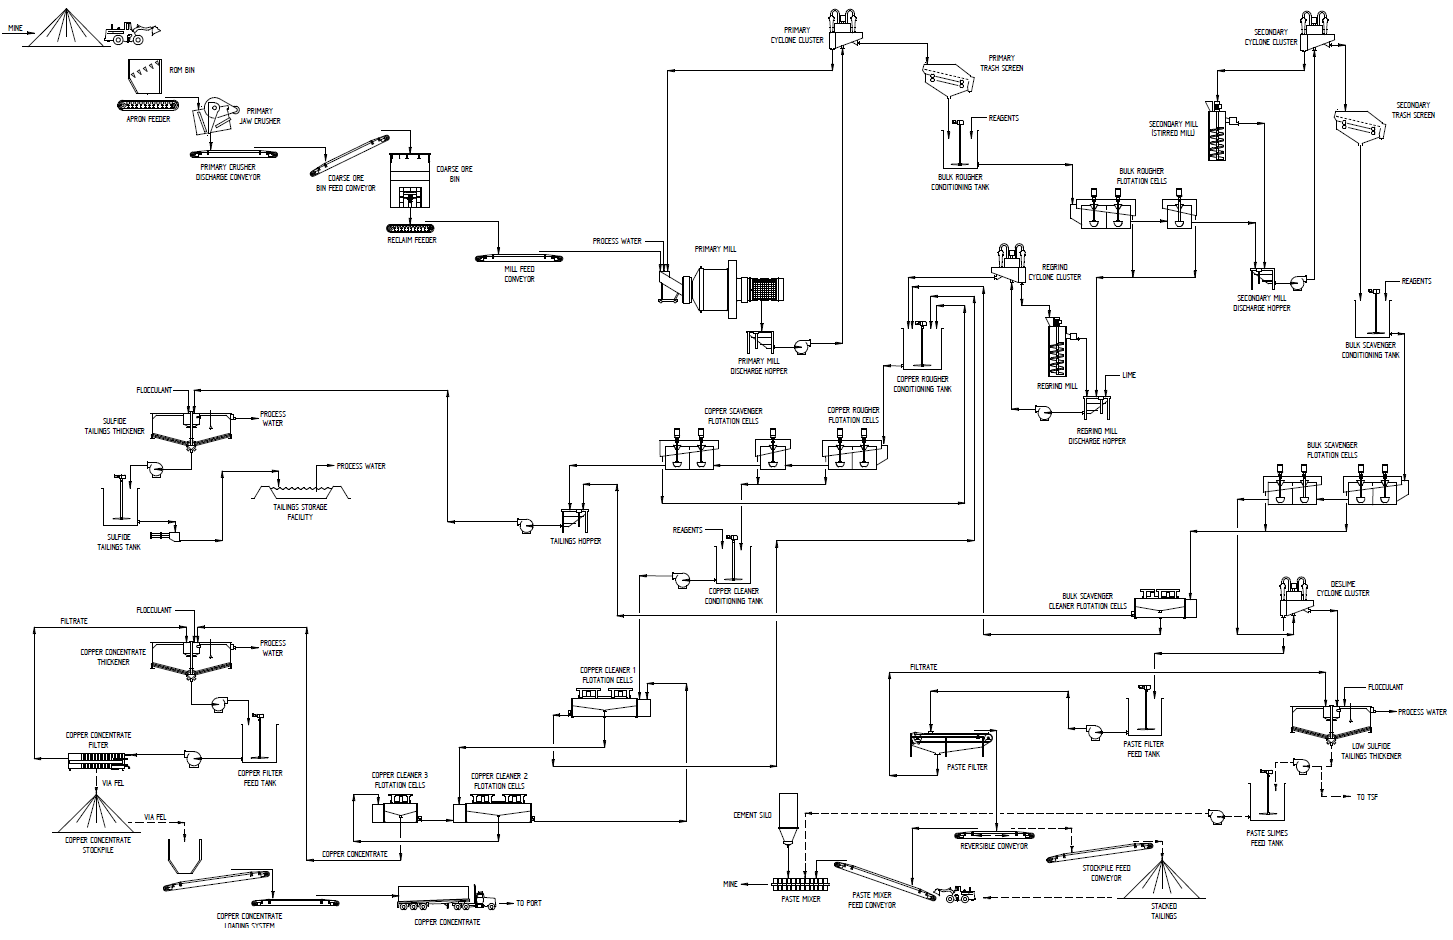
Figure 17.1 Simplified Process Flowsheet

KSM (Kerr-Sulphurets-Mitchell) — 2022 Technical Report

The 2022 Prefeasibility Study outlines the recovery methods for the KSM project, designed to process ore from the Mitchell, Sulphurets, and East Mitchell deposits. The process plant is designed to start with a nominal rate of 130,000 tpd and expand to 195,000 t/d by Year 3 of operations. The mill life is approximately 33 years, excluding production development and closure stages. The ore is transported via a train system through the MTT from the mine site to the Treaty OPC area.

KSM (Kerr-Sulphurets-Mitchell) — 2022 Technical Report Read Post »

Hod Maden Project process flowsheet:

Hod Maden Project — Pre-Feasibility Study

The Hod Maden Project Pre-Feasibility Study outlines the design of a processing plant primarily configured as a copper concentrator with significant gold recovery. The facility is designed to treat 900,000 tonnes per annum of underground ore, utilizing a single-stage crushing circuit followed by semi-autogenous grinding (SAG) and ball milling. The metallurgical strategy employs a bulk sulphide flotation circuit to recover gold and copper together, followed by differential flotation to upgrade the copper concentrate.

Hod Maden Project — Pre-Feasibility Study Read Post »

Figure 1-4: Simplified Process Flow Diagram

Graphite One Project — 2016 Technical Report (PEA)

The Graphite One Project is conceived as a vertically-integrated manufacturing operation for high-grade coated spherical graphite. The project involves mining and mineral processing at the Graphite Creek property in Alaska, followed by purification and value-added processing at a Product Manufacturing Plant located near a port. This strategy aims to minimize transport costs of raw material from Alaska while leveraging low-cost hydroelectric power for energy-intensive purification.

Graphite One Project — 2016 Technical Report (PEA) Read Post »

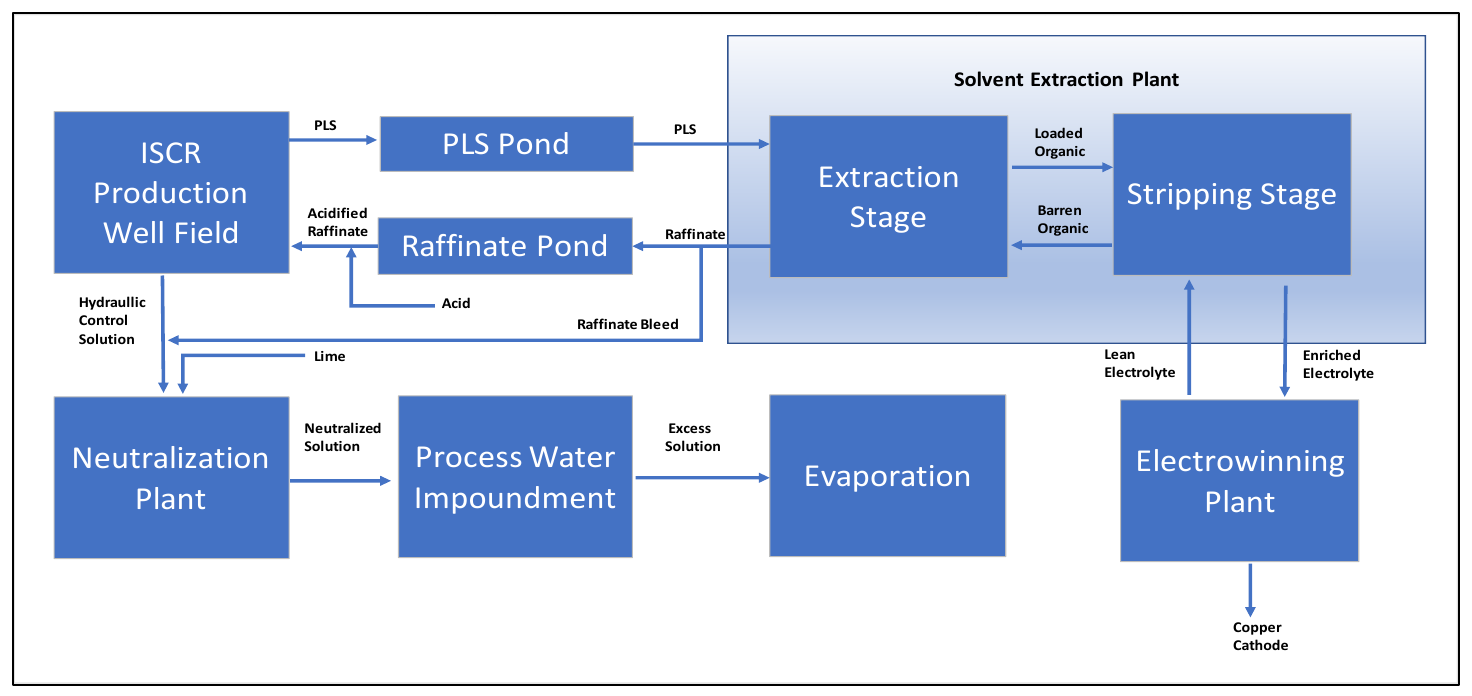
Florence Copper Project process flowsheet: Process Block Flow Diagram Prior to Rinsing

Florence Copper Project — 2023 Technical Report

The Florence Copper Project utilizes an In-Situ Copper Recovery (ISCR) method to extract copper from subsurface ore. This process involves injecting a lixiviant solution composed of approximately 99.5% water and 0.5% sulfuric acid into the orebody via injection wells. The solution dissolves copper-bearing minerals, creating a Pregnant Leach Solution (PLS) which is recovered through a network of recovery wells and pumped to a process plant.

Florence Copper Project — 2023 Technical Report Read Post »

Fremont Gold Project — 2023 Technical Report

This section details the recovery methods for the Fremont Gold Project Preliminary Economic Assessment. The project utilizes a dual processing approach based on mineralization type. Sulphide replacement mineralization (SRM) and quartz-hosted gold mineralization (QTZ) require an oxidation step and are treated via a 6,000 tonne per day flotation concentrator. Oxide cap mineralization (OCM) is amenable to heap leaching at a rate of 1,500 tonnes per day.

Fremont Gold Project — 2023 Technical Report Read Post »

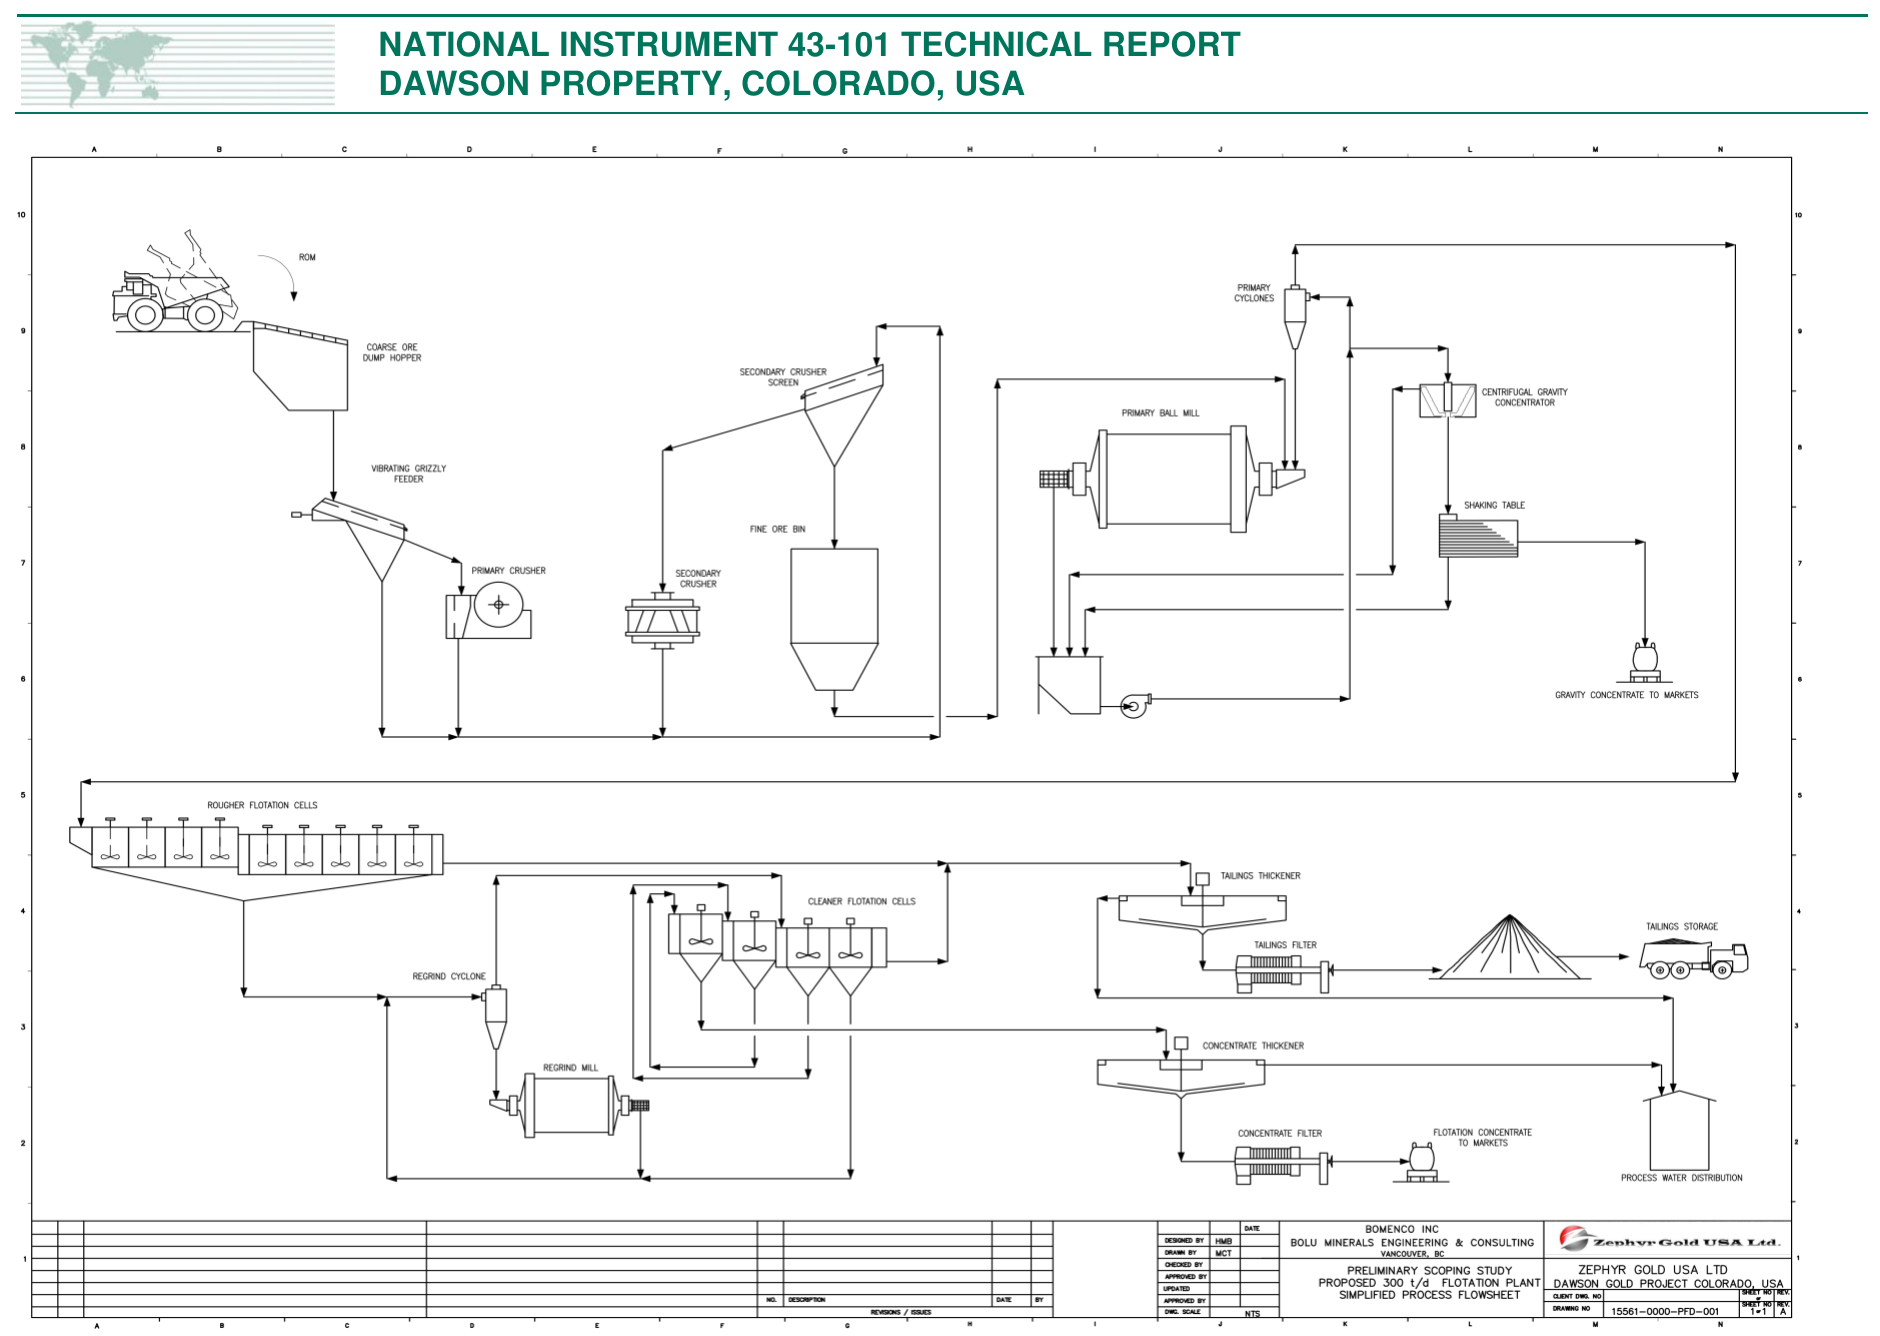
Dawson Property process flowsheet: Simplified Process Flowsheet

Dawson Property — 2017 Technical Report

This NI 43-101 Technical Report outlines the proposed process plant design for the Dawson Property located near Cañon City, Colorado. The design is based on metallurgical test results from 1991 Hazen and 2015 Inspectorate reports. The facility is designed for an annual throughput of 120,728 tonnes of Run-of-Mine (ROM) ore, operating 365 days per year with a daily nominal rate of 330.8 tonnes. The project is currently in the development phase, specifically a preliminary scoping study, with a mine life of 3.9 years.

Dawson Property — 2017 Technical Report Read Post »

Rowan PEA Crushes and Samples Ore at Site, Then Toll Mills It Through an Expanded Gravity-Leach-CIP Plant in Red Lake

This technical report outlines the recovery methods for the Rowan deposit located in the Red Lake region of northwestern Ontario. Several existing ore processing facilities in the region are capable of processing the ore as off-site toll milling options. These facilities currently operate conventional gravity-leach-CIP flowsheets, which are compatible with the metallurgical characteristics of the Rowan deposit.

Rowan PEA Crushes and Samples Ore at Site, Then Toll Mills It Through an Expanded Gravity-Leach-CIP Plant in Red Lake Read Post »

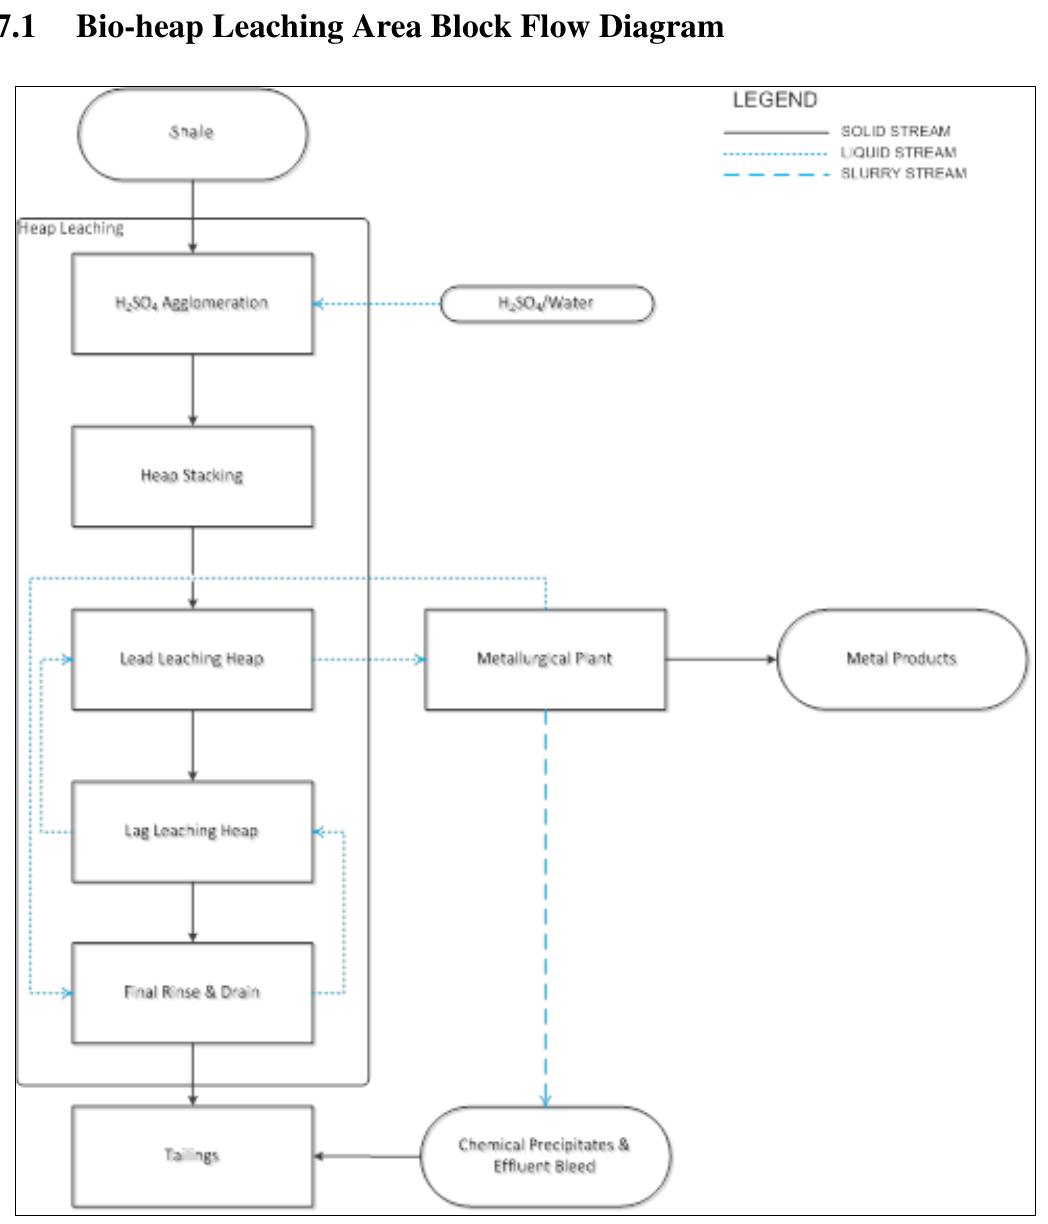
Buckton Deposit (SBH Property) process flowsheet: Bio-heap Leaching Area Block Flow Diagram

DNI Metals Inc. Buckton Deposit PEA, SBH Property, Alberta

This Pre-Feasibility Study (PEA) for the Buckton Deposit on the SBH Property in Alberta outlines a conceptual metallurgical plant designed to recover multiple metals from alum shale deposits. The primary extraction method selected is bio-heap leaching, chosen for its lower capital and operating costs per tonne compared to tank leaching, particularly suited for low-grade feed. The process utilizes coarse particle sizes to eliminate fine grinding requirements, allowing percolation of leach solution through a stationary heap to collect a low-solids pregnant leach solution (PLS). The initial screening identified Copper, Zinc, Uranium, Nickel, Cobalt, and Rare Earth Elements (REEs) as economically viable, with Lithium omitted due to processing cost constraints.

DNI Metals Inc. Buckton Deposit PEA, SBH Property, Alberta Read Post »

Scroll to Top