

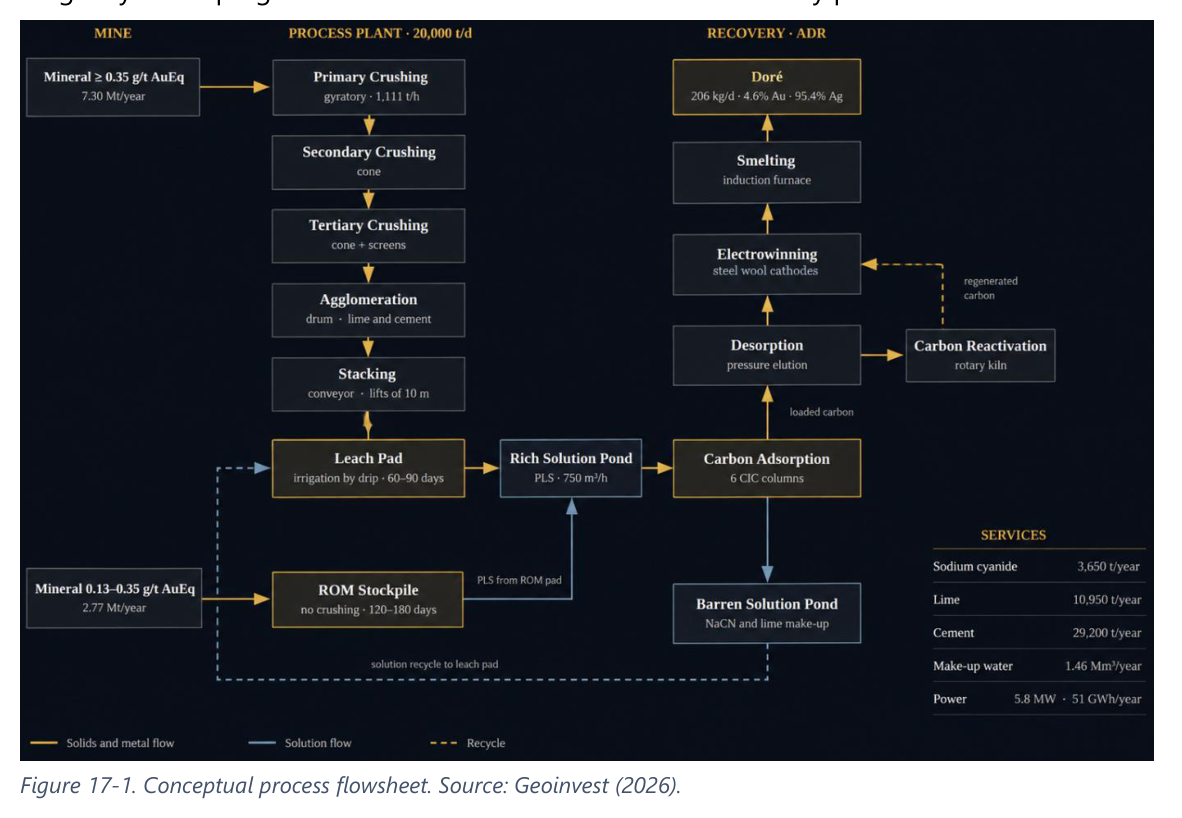
The El Dorado-Monserrat Gold-Silver Project is a PEA-stage project located in the Magallanes and Deseado Departments of Santa Cruz Province, Argentina, within the Deseado Massif. Fredonia Mining Inc. owns the project through its Argentine subsidiaries, including 5R S.A. and Minera Fredonia S.A. The project targets gold and silver from a low-sulfidation epithermal system and is advancing toward a Pre-Feasibility Study. The conceptual processing configuration comprises three-stage crushing, agglomeration, cyanide heap leaching, gold and silver recovery by adsorption on activated carbon, desorption, electrowinning and smelting to doré. A separate run-of-mine leach pad treats the intermediate-grade fraction without crushing. The design corresponds to the level of definition expected of a Preliminary Economic Assessment and remains conceptual.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Nominal plant throughput | 20,000 | t/d | 7.30 Mt per annum |
| Crushing capacity | 1,111 | t/h | At 75% utilization |
| Crushing stages | Three | Not applicable | Gyratory, secondary and tertiary cone |
| Product size (P80) | 12.5 | mm | To be confirmed by column testwork |
| Agglomeration | Rotary drum | Not applicable | Lime and cement addition |
| Lift height | 10 | m | Multi-lift permanent pad |
| Leach cycle | 60 to 90 | days | To be confirmed by column testwork |
| Irrigation rate | 10 | L/h/m² | Drip emitters |
| Area under irrigation | 75,000 to 112,500 | m² | Depending on leach cycle |
| Pregnant solution flow | 750 to 1,125 | m³/h | Depending on leach cycle |
| Adsorption | Six columns in series | Not applicable | Carbon-in-column |
| Desorption | Pressure elution | Not applicable | Hot caustic-cyanide eluate |
| ROM pad throughput | 2.77 | Mt/y | Uncrushed, longer cycle |
| Sodium cyanide consumption | 0.5 | kg/t | 3,650 t annual requirement |
| Lime consumption | 1.5 | kg/t | 10,950 t annual requirement |
| Cement consumption (agglomeration) | 4.0 | kg/t | 29,200 t annual requirement |
| Make-up water | 0.20 | m³/t | 1.46 Mm³ annual requirement |
| Power | 7 | kWh/t | 51 GWh · 5.8 MW installed |
| Process plant heap leach Au recovery | 85 | % | Benchmark and historical testwork; planning assumption |
| Process plant heap leach Ag recovery | 70 | % | Benchmark and historical testwork; planning assumption |
| ROM leach pad Au recovery | 50 | % | Expert criteria; planning assumption |
| ROM leach pad Ag recovery | 20 | % | Expert criteria; planning assumption |
Overview
The conceptual process design adopted for the Project uses three-stage crushing, agglomeration, cyanide heap leaching, gold and silver recovery by adsorption on activated carbon, desorption, electrowinning and smelting to doré. A separate run-of-mine leach pad treats the intermediate-grade fraction without crushing. Throughputs, consumption rates and equipment sizing are preliminary criteria established by benchmarking against comparable heap leach operations in the Deseado Massif and by expert criteria. They require confirmation through metallurgical testwork on representative composites and through engineering development at the next stage of study.
Historical cyanidation testwork and the preliminary bottle-roll program completed by Fredonia indicate that selected Main Veins mineralization is amenable to cyanide leaching. The available database remains limited in sample number, spatial representation, oxidation state and coverage of La Herradura. A metallurgical program on composites assembled to show the proportions of vein and host rock that will be placed on the leach pad is in progress and is required to establish recovery, reagent consumption, leach kinetics and optimum crush size.
For mine planning and economic evaluation, the recoveries have been adopted as planning assumptions. These recoveries are appropriate as preliminary planning assumptions for the PEA and require confirmation through the ongoing metallurgical program prior to the PFS. These PEA recovery assumptions are distinct from the 85% Au and 80% Ag recovery assumptions used solely in calculating AuEq for secondary Mineral Resource reporting.
Mined material above 0.35 g/t AuEq is delivered from the pits to a primary gyratory crusher. Material between 0.13 and 0.35 g/t AuEq is hauled directly to a separate run-of-mine leach pad.
Key Process Stages
Material above 0.35 g/t AuEq is reduced in three crushing stages, closing on screens, to a product size suitable for heap leaching. The crushed product is agglomerated in a rotary drum with lime and cement and wetted with barren solution, then conveyed to the leach pad and stacked in lifts. Stacked material is irrigated by drip emitters with an alkaline sodium cyanide solution. Pregnant leach solution drains through the liner collection system to the pregnant solution pond and is pumped to the recovery plant.
Gold and silver are adsorbed onto activated carbon in a series of carbon-in-column vessels. Barren solution returns to the barren pond, is reconstituted with cyanide and lime, and is recirculated to the pad. Loaded carbon is transferred to the desorption circuit, where the metals are stripped under pressure into a hot caustic-cyanide eluate. The eluate is passed through electrowinning cells fitted with steel wool cathodes, and the cathode product is smelted in an induction furnace to produce doré bars. Stripped carbon is thermally reactivated in a rotary kiln and returned to the adsorption circuit.
Material between 0.13 and 0.35 g/t AuEq is hauled directly to a separate run-of-mine leach pad without crushing or agglomeration, stacked by truck and irrigated at a lower rate over a longer cycle. Its pregnant solution is directed to the same recovery plant.
Additional Interesting Data and Summary
Applying the adopted recoveries to the plant feed gives approximately 3,469 kg of gold and 71,642 kg of silver per annum, equivalent to 9.5 kg of gold and 196 kg of silver per day. At a solution flow of 750 m³/h the pregnant solution grades approximately 0.53 mg/L gold and 10.9 mg/L silver, a silver-to-gold ratio of approximately 21 to 1. Doré production is of the order of 206 kg per day, containing approximately 4.6% gold and 95.4% silver.
Given the silver-rich solution chemistry, the PEA includes an allowance for additional recovery-circuit capacity, including the potential incorporation of Merrill-Crowe precipitation. The final recovery configuration will be selected and engineered during the PFS. For silver-dominant solutions the Merrill-Crowe process, in which the metals are precipitated with zinc dust after clarification and deaeration, is the conventional alternative. Its efficiency does not depend on the silver-to-gold ratio and it avoids the carbon loading constraint. A trade-off study between carbon-in-column and Merrill-Crowe is required before the Pre-Feasibility Study, and its outcome may modify the recovery circuit described here. The capital and operating estimates are not materially altered by that selection at the present level of definition.
Water is required for agglomeration, to compensate evaporation and solution retention within the pad, and for dust suppression and services. The current exploration water sources have not been demonstrated to meet operating-scale requirements, and a hydrogeological study is required. Power is assumed to be self-generated. Connection to the regional transmission line located approximately 17 km from the Project has not been studied.
The process concept is appropriate for the mineralization and scale of the Project and is consistent with established practice for low-sulfidation epithermal deposits in the Deseado Massif. The following matters require resolution before the concept can be relied upon: metallurgical recoveries are not supported by testwork on representative composites; the run-of-mine recoveries of 50% gold and 20% silver on uncrushed material are the least supported assumptions of the evaluation and contribute approximately 5% of annual metal production; the optimum crush size has not been established; the recovery method has not been selected; reagent consumptions are benchmark values and must be confirmed by testwork; no cyanide destruction or effluent treatment circuit has been defined; and water supply and power supply have not been established at operating scale.
Key Processes
- Three-stage crushing using a primary gyratory crusher, secondary and tertiary cone crushers, closing on screens to a P80 of 12.5 mm
- Agglomeration in a rotary drum with lime and cement addition
- Cyanide heap leaching with drip emitters on a multi-lift permanent pad using a 60 to 90 day leach cycle
- Carbon-in-column adsorption using six columns in series
- Pressure elution desorption with hot caustic-cyanide eluate
- Electrowinning with steel wool cathodes
- Smelting in an induction furnace to produce doré bars
- Thermal reactivation of stripped carbon in a rotary kiln
- Run-of-mine leaching on a separate pad for material between 0.13 and 0.35 g/t AuEq without crushing or agglomeration
Source: NI 43-101 Technical Report, Preliminary Economic Assessment, El Dorado – Monserrat Gold-Silver Project, August 17th, 2026. Project website: El Dorado – Monserrat Gold-Silver Project
