

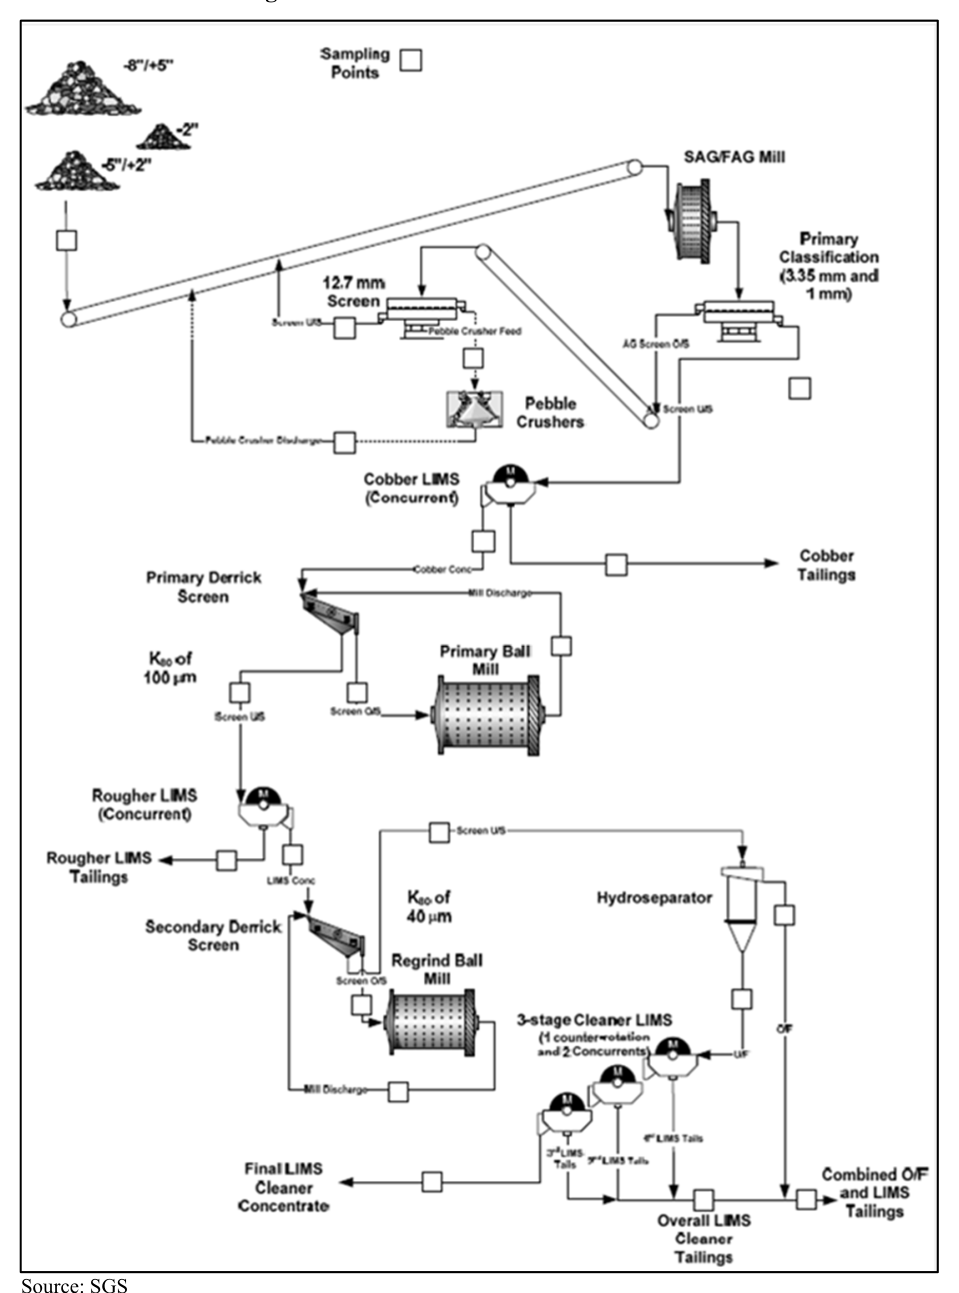
The April 2015 feasibility study for Lac Otelnuk in Nunavik, Quebec describes five gyratory crushers, five production trains with gearless SAG mills, three stages of magnetic separation and desliming to reach a 68.5% iron concentrate.
The Lac Otelnuk Project lies in the Nunavik region of Quebec, about midway north in the Labrador Trough iron range. Adriana Resources Inc. acquired the right to earn a 100% interest in the claims in 2005, and Lac Otelnuk Mining Ltd. is the project company named on the Feasibility Study NI 43-101 Technical Report, which has an effective date of March 25, 2015 and an issue date of April 23, 2015. The process plant treats magnetite ore from the open pit. The operation mills approximately 188.7 Mt/y of iron-bearing mineralization to produce 50 Mt/y of magnetite concentrate. It develops in two phases, with Phase 1 making 30 Mt/y of concentrate and Phase 2 adding 20 Mt/y. The process involves multiple grinding and milling stages followed by a conventional magnetite recovery circuit with desliming thickeners and magnetic separators to produce a pellet feed iron concentrate. The design life is 30 years.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Concentrator throughput | 188.7 | Mt/y | 23,932 t/h, both phases |
| Concentrate output | 50 | Mt/y | Phase 1 30, Phase 2 20 |
| Average feed grade | 28.7 | % Fe | 18.2% magnetite |
| Concentrate quality | About 68.5 | % Fe | Below 4% silica plus alumina |
| Davis tube weight recovery | 26.5 | % | 30-year average |
| Primary crushers | 5 | gyratory | 6,154 t/h each, 70% availability |
| Production trains | 5 | trains | Each with three 40 ft SAG mills |
| Process plant availability | 90 | % | Not applicable |
| SAG recirculating load | 30 | % | 3.35 mm screen |
| Cobber / rougher / cleaner field | 1,150 / 1,000 / 900 | gauss | At 50 mm |
| First / second stage ball mill recirculation | 250 | % | Work indices 14.8 / 17.5 kWh/t |
| Final grind | 48 | µm D80 | Pilot plant |
| Concentrate thickener underflow | 67 | wt% | 1,269 t/h per train |
| Tailings thickener underflow | 60 | wt% | 2,829 t/h per train |
| ROM stockpile | 16 | h | Between mine and plant |
Overview
Ore is crushed in gyratory crushers and stockpiled for 16 hours. Five parallel trains each feed three gearless SAG mills in closed circuit with 3.35 mm screens. Cobber magnetic separators at a transfer size of 700 to 800 microns balance load between the SAG mill and the first ball mill. Two stages of ball milling are separated by a roughing magnetic separation, and a desliming thickener sits ahead of three-stage cleaner separators. The final product is thickened and held in slurry storage tanks ahead of a product delivery system, and tailings are thickened for disposal.
Key Process Stages
Primary crushing
Five large-capacity gyratory crushers are planned, three in Phase 1 and two more in Phase 2, with a crusher work index of 19.9 kWh/t and a maximum feed size of 1,321 mm. Each pocket has 688 t of live capacity for two trucks, and a 24-hour emergency stockpile is provided.
SAG milling and cobbing
Each of the five trains uses three parallel 40-foot SAG mills with gearless drives, the largest currently proven size. The SAG mills take a maximum 15% ball load, and a 10% safety factor on throughput is applied. Specific power is 12.9 kWh/t. Cobber magnetic separation uses single-drum counter-rotation low-intensity magnetic separators (LIMS). Cobber concentrate weight recovery was 71.2% in bench-scale testwork against 47% in the pilot plant, so no safety factor was added for the first-stage ball mill.
Ball milling and rougher separation
Fine grinding is a two-stage ball mill arrangement separated by a roughing LIMS stage. Each train has two gear-driven first-stage ball mills and one large second-stage ball mill with a wraparound motor, which was preferred over two smaller gear-driven ones. A rougher concentrate weight recovery of 64.3% from bench tests is close to the pilot average of 62.6%, and a 10% safety factor applies to the second-stage mill. A final grind of 48 µm D80 gave good concentrate in the pilot plant.
Desliming and cleaning
Initial testing showed a heavy loading of slimes in product after a three-stage cleaner LIMS, so a desliming thickener was added ahead of the cleaners. Triple-drum counter-current LIMS follow conventional practice for cleaning. In the metallurgical mass balance, cobber concentrate takes 71.2% of the feed weight and 98.2% of the magnetic iron, rougher concentrate 45.78% of feed, slimes 15.79%, and final concentrate 26.5% of feed weight at 69.10% Fe, with 95.5% magnetic iron recovery.
Thickening
Concentrate is thickened to 67% solids and tailings to 60%, with product thickeners handling 1,269 t/h per train and tailings thickeners 2,829 t/h. Slurry storage tanks and pump stations feed a product delivery system.
Additional Interesting Data and Summary
Magnetite weight recovery is critical, because any hematite in the ore is not recovered by the process. Laboratory concentrate from SGS Lakefield reached 69.0% Fe, 2.95% silica and 0.01% sulphur. Ore feed is about 45% silica with 2.64% magnesia and 3.09% lime.
The plant is sited on solid bedrock about 4 km west of the pit, within the claim boundaries but not on top of potential mineral resources. Water comes from a pond about 2 km upstream, an airstrip is about 12 km away, and design criteria require a safe working facility for subarctic conditions, with attention to prevailing winds, snow accumulation and cold air infiltration. The plant runs 24 hours a day, seven days a week, and the bench-scale testwork behind the flowsheet used a 30-year composite sample representing the average mine plan feed. JKSimMet simulation confirmed pilot plant data, with adjustments for a coarser industrial feed.
Key Processes
- Gyratory crushing
- Gearless SAG milling in closed circuit with screens
- Cobber, rougher and cleaner low-intensity magnetic separation
- Two-stage ball milling
- Desliming thickening
- Concentrate and tailings thickening
Source: Lac Otelnuk Project Feasibility Study – NI 43-101 Technical Report, April 23, 2015.
