

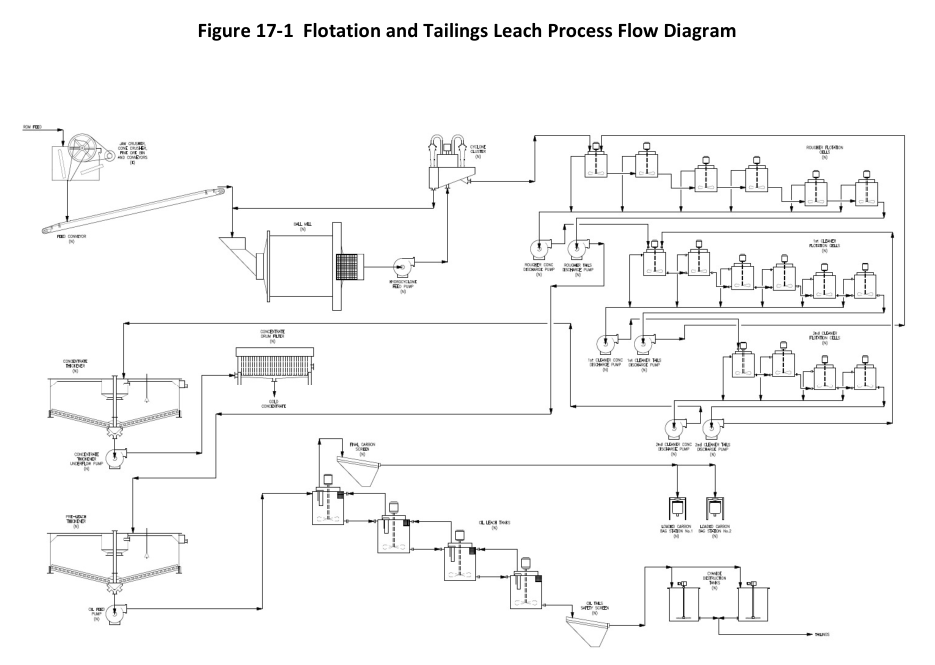
The Copperstone project in La Paz County, Arizona, is a gold project owned by Mining Americas Inc. (formerly Minera Alamos Inc.). A Preliminary Feasibility Study has been completed with an effective date of May 27, 2026. The project is being developed as a restart of previous operations. The source material does not state expected construction timing.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Target commodity | Gold | Not applicable | Not stated |
| Plant feed rate (initial) | 600 | Average tons per day | Design value |
| Design capacity | 1000 | Shorts tons per day | Design value |
| Plant availability | 92 | % | Design value |
| Bond work index | 14.2 | kWh/st | Test result |
| Grind size (P80) | 120 (125) | Mesh (microns) | Design value |
| Flotation mass pull | ~4 | % | Design value |
| Pre-leach thickener underflow density | 45 | Wt% | Design value |
| Leach residence time | 24 | hr | Design value |
| Tailings feed percent solids | 40 | Wt% | Design value |
| Raw water requirement | 100 to 200 | gpm | Design value |
| Average power demand | 3 | MW | Design value |
| Combined gold recovery | ~96 | % | Test result |
| Gold recovery via flotation concentrate | 75-80 | % | Test result |
| Gold recovery via CIL of tailings | 85-90 | % | Test result |
Overview
Process selection for the Copperstone deposit was based on historical metallurgical testing. The chosen flowsheet combines crushing and grinding with flotation to produce a high-grade gold concentrate for off-site processing. A second circuit leaches the flotation tailings using bulk cyanide in a carbon-in-leach (CIL) operation. This hybrid approach was selected following economic and technical analysis as the best processing option for the deposit.
The proposed flowsheet takes advantage of existing equipment including a primary crusher, secondary crusher, screen, ore bin, and conveyors. This equipment is currently being refurbished. The remaining processing plant will be reconstructed using sourced equipment. Initial throughput capacity averages 600 tons per day, with the potential to expand up to 900 tons per day once operations are underway.
The existing ball mill will be removed and replaced with a larger mill to achieve the target throughput and grind size for the flotation circuit. A pre-leach thickener is included in the design, followed by four leaching tanks providing 24 hours of total residence time. Space allows for additional expansion in the future. Loaded carbon product will be batch screened, separated, and bulk-bagged for off-site processing.
Testwork results indicate an overall combined gold recovery of approximately 96%. The gold flotation circuit accounts for 75-80% of that recovery, and the CIL circuit recovers 85-90% of the remaining gold from the flotation tailings. Flotation concentrates are shipped offsite to a third-party processor for toll processing and gold recovery.
Key Process Stages
The process plant will restart using existing infrastructure from previous operations where available. Run-of-mine ore is delivered to the jaw crusher feed hopper either directly from the mine or by loader from stockpiles near the crushing plant. Jaw crusher discharge goes to a crusher screen operating in closed circuit with a cone crusher. Screened product is conveyed to a crushed ore bin, from which a conveyor feeds an 11-foot by 15-foot primary ball mill with a 1000 horsepower motor. The ball mill operates in closed circuit with hydro-cyclones, reducing ore to a maximum nominal P80 of 100 to 125 microns (120 to 150 mesh). The plant operates with an overall design availability of 92%.
Cyclone overflow feeds a conditioning tank and then a flotation circuit with roughers and two stages of cleaning. This produces a high-grade gold concentrate with a mass pull of up to 4%. The gold concentrate is dewatered in a thickener. Thickener underflow at 50% solids is pumped to a plate-and-frame filter for discharge onto a concrete pad. From there it goes to bulk container loading and shipment off-site.
Flotation tailings go to a tailings pre-leach thickener to remove excess water ahead of cyanide leaching. Thickener underflow is pumped at 45% solids to the CIL tanks. Slurry combines with cyanide solution from the pre-mixed reagent holding area. Dissolved gold is recovered through counter-current solution flow and intermittent carbon advancement in the CIL tanks. Mixing interstage screens separate slurry from the coarser carbon while allowing solution contact for loading. Loaded carbon is screened, drained, and bagged for stripping and refining off-site.
Leached tailings are pumped to a detoxification stage where cyanide destruction occurs via SMBS and aeration before being discharged to the existing tailings storage facility. Recovered process solution returns to the plant.
The plant site plan uses standard two-stage crushing followed by closed circuit ball mill grinding with a gravity circuit placed in the cyclone underflow. Initially the plant operates at a maximum of 600 tons per day, producing approximately 20 tons of flotation concentrate at 4 to 8 ounces per ton. A gravity circuit may be introduced in the future if required, potentially producing a concentrate up to 15 ounces per ton. The new CIL leaching plant will be constructed north of the existing plant footprint next to the flotation plant location.
Additional Interesting Data and Summary
The process plant operates 24 hours per day, 7 days per week. Initial run-of-mine feed is 219,000 tons per year. ROM specific gravity is 3.17 pounds per cubic foot. ROM F80 is 3.5 inches. The crushing plant operates at 100 tons per hour for 12 hours per day. The fine ore bin holds 500 tons. Processing mill F80 is 0.5 inch.
The pre-leach thickener design settling rate is 295 square feet per ton per day. Leach tank feed specific gravity is 1.45.
Blowers supply low pressure process air to the flotation cells. Compressors supply medium pressure process air to the CIL tanks if required. Air compressors provide plant and instrument air. Plant air receivers act as a buffer storing air to account for variations in demand. Instrument air is dried before storage and distribution.
Water for the gland seal system comes from the raw water tank. The gland seal water tank stores and distributes gland water with pumps in a duty-standby configuration. Water feeding the gland water tank passes through 25-micron particulate filters to prevent damage to gland seals.
Process water consists of concentrate thickener overflow, flotation tailings thickener overflow, tailings reclaim water, and fresh makeup water as required. Process water is stored in a storage tank and distributed by pumps in a duty-standby configuration to points in the grinding and flotation circuits.
Water is sourced from reclaim water from the TSF polishing pond, underground development discharge water, or three locally drilled water wells.
Power for the process plant and the rest of the project comes from grid power. Average power demand for the process plant is approximately 3 MW.
Plant feed and tailings products will be sampled manually for an accurate metal balance. A weigh scale on the ball mill feed conveyor measures primary crushed material tonnage. A manual belt cut sampling point on the ball mill feed conveyor allows collection of a mill feed head grade sample for cross-validation. This sample also determines and reviews moisture content. Water supplied and used in various areas is continuously monitored.
Metallurgical samplers generate shift composite samples for plant accounting. Process streams with metallurgical samplers include cyclone overflow, flotation concentrate, flotation tailings, and CIL tailings. Reagent usage rates are measured and accumulated hourly using flowmeters. Reconciliation over longer periods uses delivery receipts and stock takes.
Grinding and crushing liners and grinding media consumption rates are specified. Jaw crusher liners are consumed at 1 set per year. Cone crusher liners are consumed at 1 set per year. Ball mill liners are consumed at 1.5 sets per year. Grinding media consumption is 1.25 pounds per ton of feed.
Reagent storage, mixing, and pumping facilities are located in designated areas near the flotation and leaching circuits. Flotation reagents include PAX collector at 0.165 pounds per ton, MIBC frother at 0.45 pounds per ton, and R208 at 0.085 pounds per ton. Leaching reagents include cyanide as NaCN 20% at 2 pounds per ton, hydrated lime at 90% Ca(OH)2 w/w at 2.5 pounds per ton, SMBS at 0.5 pounds per ton, and flocculant at 0.3 pounds per ton.
Key Processes
- Two-stage crushing using a primary jaw crusher and secondary cone crusher
- Closed circuit ball mill grinding with hydro-cyclones
- Rougher flotation with two stages of cleaning
- Concentrate thickening and filtration
- Pre-leach thickening of flotation tailings
- Carbon-in-leach cyanidation with four tanks
- Cyanide destruction via SMBS and aeration
- Loaded carbon screening and bagging for off-site processing
Source: National Instrument 43-101 Technical Report: Preliminary Feasibility Study for the Copperstone Project, La Paz County, Arizona, USA, September 2, 2026. Project website: Copperstone Project
Consolidated report summaries
The following former standalone pages about this operation were consolidated here on October 25, 2026. They are retained for source traceability; dates and figures reflect each report’s own effective date and may be superseded by the current information above.
Kerr Mines Inc. — Copperstone Project NI 43-101 Technical Report
Whole ore leaching was selected as the base case processing option for the Copperstone project based on 97 percent gold recovery, elimination of smelter charges, and superior economic results relative to flotation alternatives.
Kerr Mines Inc. commissioned new metallurgical testwork for the Copperstone deposit through Resource Development Inc, with the dual purpose of confirming prior metallurgical results and evaluating processing options. Testing compared three process routes: flotation producing a gold concentrate, and two additional options that produce a doré bar as the final saleable product. The ability to produce a doré bar was identified as considerably advantageous from an offtake revenue perspective compared with selling a gold concentrate.
Test results indicated that whole ore leaching achieved 97 percent gold recovery, while the other processes achieved recoveries of 88 to 90 percent. Based on economic and technical analysis, whole ore leaching was selected as the preferred processing option. Although operating costs for whole ore leaching were the highest of the three options, the increase in recoveries and elimination of smelter charges made this option economically superior. The whole ore leach process was selected as the base case scenario, with the process flow sheet described with reference to Carbon-in-Pulp.
Processing is planned for 840 tons per day on a 5-day per week schedule, which coincides with the 7-day per week mining plan. The process uses the existing crushing circuit, with ore conveyed to the ball mill where it is ground to P80 minus 200 mesh in a closed-circuit arrangement. The whole ore leach process can also be readily modified to incorporate a SART process to produce copper as a by-product and reduce cyanide consumption in the leach process.
The existing flotation plant will be modified, with some equipment eliminated as additional testwork and process plans dictate. Based on gravity testing and Work Index testing, certain existing equipment will not be needed and will be removed from the circuit, including the Knelson concentrator and rod mill. The new process will use the existing crushing circuit conveyed to the ball mill, and the design criteria specify that the plant can operate two days a week extra when required, or downtime will be utilized for maintenance.
The current plan is to construct the leach plant to the north of the existing flotation plant. Startup water for the plant is estimated at 350 gpm, with operating consumption estimated at 52 gpm. Ongoing testing indicates that intermittent copper in the ore feed may necessitate precipitation of copper through additional processing steps, which would recycle free cyanide back to the leach circuit and reduce overall cyanide consumption. This would keep overall cyanide consumption for gold ore leaching at or below design parameters. Testing for this is ongoing and would likely necessitate one additional 9 ft by 9 ft leach tank and a small filter press. The presence of intermittent copper in the ore feed may also necessitate the need for one additional leach tank and a small filter press.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Gold recovery, whole ore leach | 97 | % | Test result |
| Gold recovery, other options | 88 to 90 | % | Range across two flotation options |
| Design tonnage | 600 | tpd/week | Based on 5-day per week plant operation |
| Design tonnage per 5 days | 840 | tpd | Equivalent to 35 tph |
| Plant operation | 5 | days/week | Mine operates 7 days per week |
| Plant availability | 100 | % | Design criterion |
| Run-of-mine ore | P80 of 4 | inch | Feed specification |
| Secondary crusher product | P80 of 3/8 | inch | Feed specification |
| Ball mill Bond Work Index average | 14 | Not stated | Closed size of 100 mesh |
| Ball mill Bond Work Index maximum | 18 | Not stated | Closed size of 100 mesh |
| Ball mill Bond Work Index low | 11 | Not stated | Closed size of 100 mesh |
| Ball mill product P80 | 200 | mesh | For Options 1 and 2 |
| Ball mill product P80 | 150 | mesh | For Option 3 |
| Ball mill discharge P80 | 150 | mesh | Whole ore leach design |
| Leach tank diameter | 9 | ft | 9 ft by 9 ft high with agitators |
| Leach tank height | 9 | ft | 9 ft by 9 ft high with agitators |
| Number of leach tanks | 6 | count | Additional tank may be required for SART integration |
| Tailing thickener diameter | 20 | ft | Unit area of 3 ft²/st/24hrs |
| Tailing thickener unit area | 3 | ft²/st/24hrs | Design criterion |
| Tailing throughput | 840 | tpd | Design criterion |
| Startup water | 350 | gpm | Estimated |
| Operating water consumption | 52 | gpm | Estimated |
| Abrasion index values | 0.0259 to 0.359 | Not stated | Range from testwork |
Overview
The Copperstone project involves reopening and modifying an existing processing facility to treat ore through a whole ore leach flowsheet. The project required removal of some existing equipment and installation of additional equipment specific to the whole ore leach process. This included removing a rod mill, Knelson concentrator, jig, Knelson screen, and associated pumps, along with a dryer and flotation cells, and adding leach tanks and a thickener. The design criteria established a plant availability of 100 percent, with grinding to P80 of 150 mesh for the whole ore leach option.
The project site location for the whole ore leach plant is to the north of the existing flotation plant. The existing equipment list included gravity concentration equipment, which the testwork indicated would not be needed because the deposit does not have free coarse gold. Testwork also provided data for Bond Ball Mill Work Index testing and abrasion testing, with samples representing both softer and harder material.
Key Process Stages
The existing crushing circuit will be used, with ore conveyed to the ball mill. Grinding will occur in closed circuit to achieve the target product size. The whole ore leach process will use Carbon-in-Pulp technology for gold recovery, with six leach tanks each 9 ft in diameter by 9 ft high. The leached residue will be sent to a 20 ft diameter tailing thickener with a unit area of 3 ft²/st/24hrs at a throughput of 840 tpd.
The process has provision for SART integration to treat intermittent copper in the ore feed. The SART process would precipitate copper and recycle free cyanide back to the leach circuit. This would reduce overall cyanide consumption and keep it at or below design parameters. Ongoing testwork is evaluating this option, which would require one additional leach tank and a small filter press.
The flotation plant will be modified, with equipment eliminated as additional testwork and process plans dictate. If flotation of copper from leach tails is proven economical, some existing equipment may be retained. As testwork progresses and required processing is finalized, the elimination of surplus equipment will be defined.
The existing equipment list includes jig and centrifugal gravity equipment for recovery of coarse gold, but current ongoing testwork indicates the deposit does not have free coarse gold. Some equipment will be removed from the circuit, including the Knelson concentrator and rod mill.
Additional Interesting Data and Summary
The project economics for whole ore leaching were superior despite having the highest operating costs, due to higher recovery and elimination of smelter charges. The block flow sheet for the whole ore option notes that CIP refers to Carbon-in-Pulp. The SART process integration is at early stages of evaluation, with copper not currently classified as a recoverable mineral resource according to any standard. Metallurgical testing for economic extraction of copper was ongoing but incomplete, and the study provided no certainty that copper extraction would be economically viable.
The list of major equipment with specifications and projected throughput was provided in the technical report. The additional equipment required for the whole ore leach process included leach tanks, thickener, and ancillary equipment. The removal of equipment and the projected throughput of existing equipment were specified in the report tables. The planned process plant layout was shown in Figure 17-2, with the leach plant constructed to the north of the existing flotation plant.
A review of the existing plant equipment identified that the rod mill, Knelson concentrator, jig, Knelson screen, and associated pumps were not required for the new flowsheet. These were removed from the circuit to be replaced by the whole ore leach equipment. The existing flotation cells would be modified or eliminated as required by the final process design. The plant power requirements and major consumables were detailed in the technical report tables.
Key Processes
- Whole ore leaching with Carbon-in-Pulp gold recovery
- Crushing and grinding in existing circuit with minor modifications
- Closed-circuit ball mill grinding to P80 of 150 mesh
- SART process integration for copper by-product recovery and cyanide reduction
- Existing flotation plant modification with equipment removal
- Tailing thickening in a 20 ft diameter thickener
- Removal of rod mill, Knelson concentrator, jig, and associated equipment
Source: Kerr Mines Inc. NI 43-101 Technical Report, Copperstone Project Recovery Methods, May 18, 2018.
Project website: Kerr Mines Inc., Copperstone Project NI 43-101 Technical Report
Copperstone Project — 2023 Technical Report
The Copperstone process plant design adopts whole ore cyanide leaching based on metallurgical testwork that indicated 97% gold recovery, using existing crushing and grinding equipment supplemented by new leaching and solution recovery circuits.
Report context
This technical report, dated August 2, 2023, documents the process design for the Copperstone Project. The report presents design criteria for a processing rate of 592 tonnes per day (652 short tons per day) based on mine delivery of 198,560 tonnes of mineralized material per year (219,000 short tons per year). Plant availability is set at 92%, with operations 24 hours per day, 7 days per week.
Processing route
Flowsheet selection
Metallurgical testing evaluated three process options: grinding and flotation to produce a gold concentrate; grinding, flotation, and cyanide leaching of the gold flotation concentrate; and grinding and whole ore cyanide leaching. The final two options produce doré bars. Testwork conducted by RDI for screening these flowsheet options indicated 97% recovery of gold for whole ore leaching, while the other processes achieved 88% to 90% recovery. Based on economic and technical analysis, whole ore leaching was selected as the best processing option. The report notes that although operating costs for whole ore leaching are the highest of the three options, the increase in recoveries and elimination of smelter charges make this option economically superior.
Crushing and grinding
The flowsheet takes advantage of existing equipment including the primary crusher (jaw), secondary crusher (cone), screen, ore bin, conveyors, and ball mill. This equipment will be refurbished prior to commissioning. The target grind size is 104 µm (cyclone overflow P80). The existing ball mill is larger than required for the target 600 short tons per day throughput and will operate with reduced steel load and lower power. The existing Hardinge ball mill has a motor power of 700 hp, operates at 75% of critical speed, uses 3-inch diameter balls, and has a ball charge of 25% to 35%. A single new 20-inch cyclone is specified, with a design circulating load of 250%.
Whole ore leaching
The new whole ore leaching circuit includes a pre-leach thickener followed by four leaching tanks. The pre-leach thickener is a new high-rate unit with a diameter of 6.1 m (20 ft) and a settling rate of 295 ft²/tons per day, producing an underflow density of 45 wt%. The four leach tanks each have an operating volume of 258 m³ (68,150 gallons), with a height of 30 ft and diameter of 20 ft. Total residence time with four tanks is 27.2 hours, and with three tanks is 20.4 hours. Free board is 10%. Design sodium cyanide concentration is 1,750 ppm, with design consumption of 4.3 lbs per short ton (2.15 kg per tonne).
Solution recovery and Merrill Crowe
Pregnant solution is recovered through four CCD thickeners operating in countercurrent decantation. The CCD thickeners have a diameter of 6 m (20 ft), a settling rate of 0.04625 m²/tonnes per day (0.452 ft²/tons per day), and produce underflow density of 50 wt%. The wash ratio is 2.3 based on barren to feed solids and 2.7 based on barren to feed aqueous.
Pregnant solution is processed in a Merrill Crowe circuit to precipitate gold, silver, and copper. Design feed to Merrill Crowe is 383 gpm (87 m³/hr), with a design maximum of 459 gpm (104 m³/hr). Pregnant solution grades are: Au 1.82 g/m³, Ag 0.12 g/m³, Cu 262 g/m³, and CN 383 g/m³. Zinc consumption is 36 kg/hr. The pregnant solution tank has 0.67 hours residence time with a volume of 58 m³. The barren solution tank has 2 hours residence time with a volume of 174 m³.
Following precipitation, the product will be batch leached with acid in the gold room to extract residual copper, which can be recovered using a cementation process, prior to smelting and pouring doré bars.
Detoxification
A detox tank is specified with a feed of 50 wt% solids and 4 hours residence time. The tank volume is 128 m³. Sodium metabisulfite (SMBS) consumption is 0.248 lb/ton (0.497 kg/tonne).
Key reported parameters
| Parameter | Unit | Design Value | Basis |
|---|---|---|---|
| Plant throughput | tonnes per day | 544 | Plant tonnage |
| Plant throughput | short tons per day | 600 | Plant tonnage |
| Plant availability | % | 92 | Operating basis |
| Design capacity | tonnes per day | 592 | Design |
| Design capacity | short tons per day | 652 | Design |
| ROM F80 | mm | 102 | Design |
| ROM specific gravity | , | 3.18 | Design |
| Milling feed F80 | µm | 12,500 | Design |
| Bond ball mill work index (average) | kWh/t | 13.94 | Testwork |
| Bond ball mill work index (maximum) | kWh/t | 18.03 | Testwork |
| Bond ball mill work index (minimum) | kWh/t | 10.04 | Testwork |
| Cyclone overflow P80 | µm | 104 | Design |
| Circulating load | % | 250 | Design |
| Pre-leach thickener diameter | m (ft) | 6.1 (20) | Design |
| Pre-leach thickener underflow density | wt% | 45 | Design |
| Leach tanks, quantity | , | 4 | Design |
| Leach tanks, residence time (4 tanks) | hr | 27.2 | Design |
| Leach tanks, residence time (3 tanks) | hr | 20.4 | Design |
| Leach tank operating volume (each) | m³ (gal) | 258 (68,150) | Design |
| Sodium cyanide concentration | ppm | 1,750 | Design |
| Sodium cyanide consumption | lb/st (kg/t) | 4.3 (2.15) | Design |
| CCD thickeners, quantity | , | 4 | Design |
| CCD thickener diameter | m (ft) | 6 (20) | Design |
| CCD thickener underflow density | wt% | 50 | Design |
| Merrill Crowe feed | gpm (m³/hr) | 383 (87) | Design |
| Merrill Crowe feed (design maximum) | gpm (m³/hr) | 459 (104) | Design |
| Merrill Crowe pregnant solution Au | g/m³ | 1.82 | Design |
| Merrill Crowe pregnant solution Ag | g/m³ | 0.12 | Design |
| Merrill Crowe pregnant solution Cu | g/m³ | 262 | Design |
| Merrill Crowe zinc consumption | kg/hr | 36 | Design |
| Detox tank residence time | hr | 4 | Design |
| Detox tank SMBS consumption | lb/ton (kg/tonne) | 0.248 (0.497) | Design |
Project website: https://www.sabre.gold/projects/copperstone/
Technical qualifications
The report states that testwork results indicated 97% recovery of gold for whole ore leaching, while the other processes achieved 88% to 90% recovery. Testing was conducted by RDI for screening these flowsheet options. The present testwork indicated that the deposit does not have free coarse gold. Samples representing softer and harder material were tested for Bond's Ball Mill Work Index at a closed size of 100 mesh, yielding BWi values of 10.74 kWh/ton.
The existing ball mill is larger than required for the target throughput and will operate with reduced steel load and draw lower power. The crushing and grinding circuit is currently in place and will require only minor modification, with equipment to be refurbished prior to commissioning.
Dr. Deepak Malhotra visited the Copperstone property in February 2018 and reviewed the plant flowsheet and equipment in the plant.
—
*Source: Copperstone Project , 2023 Technical Report, August 2, 2023, Sections 17.1–17.3*
