

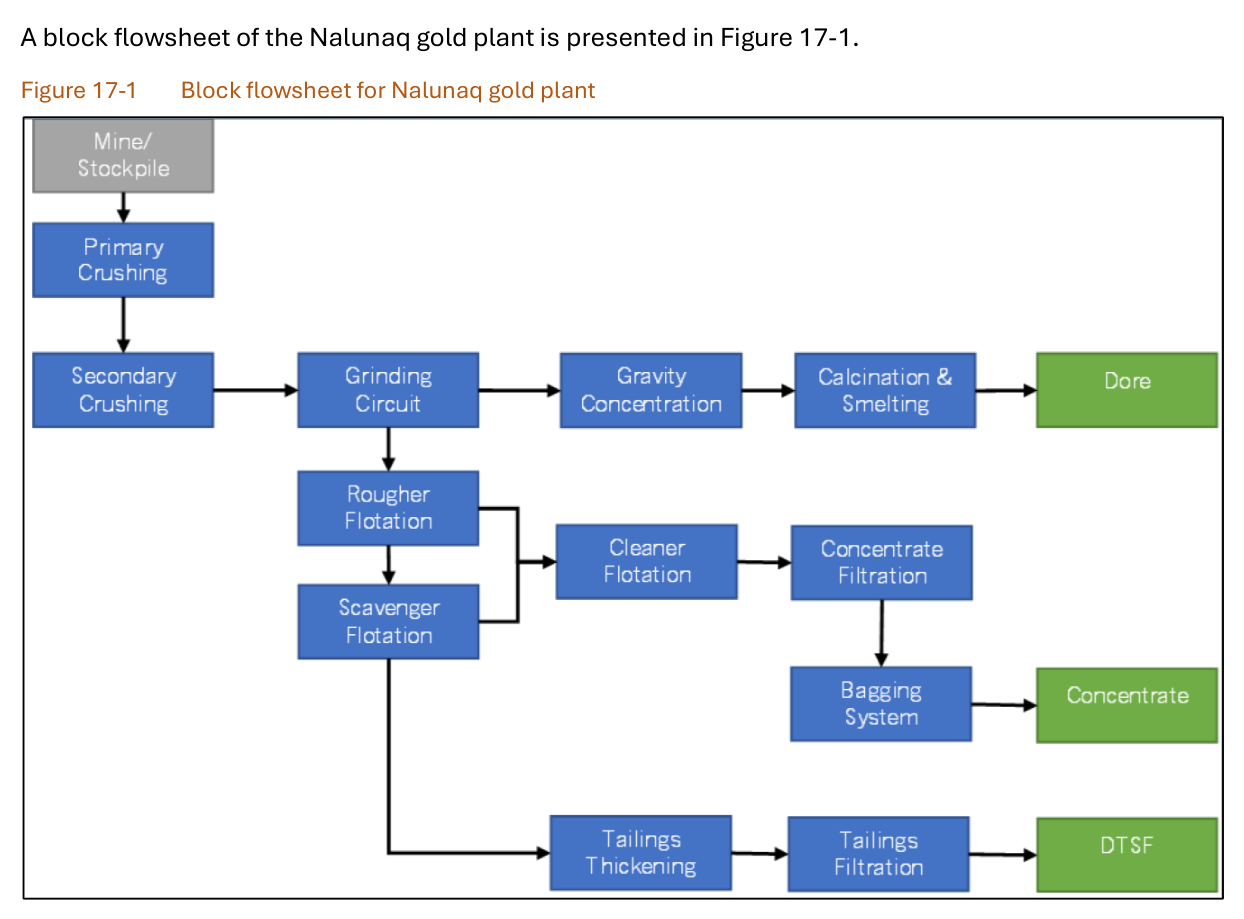
Amaroq Ltd operates a pilot-scale processing plant at the Nalunaq Gold Mine in southern Greenland, using a gravity and flotation flowsheet to produce doré and flotation concentrate.
Opening Background
The Nalunaq Gold Mine is an advanced-stage, producing underground gold operation located in southern Greenland, within the Municipality of Kujalleq, approximately 33 km northeast of Nanortalik. The project is held under exploitation licence MIN 2003-05 by Nalunaq A/S, a wholly owned Greenlandic subsidiary of Amaroq Ltd. Gold was first identified at Nalunaq in 1992, with commercial underground mining carried out from 2004 to 2013, producing approximately 367,130 ounces of gold. The mine was placed on care and maintenance following Angel Mining’s insolvency in 2013. Amaroq acquired the project in 2015-2016 and recommenced development-phase mining in 2024. Processing is via gravity concentration followed by flotation, commissioned June 2026, with a nameplate throughput of 300 tpd.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Plant type | Pilot-scale | Not applicable | Process plant treating ROM from mining activity |
| Design throughput | 12.5 | tph | ROM feed, dry basis |
| Design annual throughput | 104,025 | tpa | Dry basis |
| Design availability | 95 | % | Plant design criterion |
| Grinding circuit nominal capacity | 300 | tpd | Fresh feed, at assumed 95% availability |
| Design feed grade (gold) | 12.0-20.0 | g/t Au | ROM feed |
| Design feed grade (silver) | 1.8-3.0 | g/t Ag | ROM feed |
| Design metallurgical recovery | 94 | % Au | Design criterion |
| Flotation feed p80 | 75 | µm | Produced by classifying cyclone |
| Final flotation concentrate grade | 300 | g/t Au | Nominal |
| Final flotation concentrate arsenic | 3-4 | % As | Nominal |
| Final flotation concentrate moisture | 9 | % | After horizontal pressure filter |
| Concentrate thickener solids | 45 | % | Approximate |
| Final flotation concentrate production | 0.2-0.5 | dry tpd | Planned range |
| Gravity concentrate grade | 3,890 | g/t Au | Nominal, feed to gravity tables |
| Gravity concentrate grade | 581 | g/t Ag | Nominal, feed to gravity tables |
| Gravity concentrate processing capacity | 6 | tpd | Gold room capacity |
| Smelting batch size | 27 | kg | Typical lot size |
| Smelting frequency | Once every two days | Not applicable | Induction furnace |
| Crushed ore stockpile capacity | 900 | tonnes | Not stated |
| Feed hopper live capacity | 15 | tonnes | Not stated |
| Grizzly aperture | 250 | mm | Stationary grizzly |
| Jaw crusher feed oversize | +150 | mm | Oversize fraction |
| Classifying screen apertures | 35 and 19 | mm | Double-deck screen |
| Primary ball mill power | 330 | kW | Not stated |
| Primary ball mill dimensions | 2.1 m Ø x 6.1 m | m | EGL (effective grinding length) |
| Classifying screen aperture | 2 | mm | Ball mill closed circuit |
| Rougher flotation cells | 16 | cells | Two parallel banks of eight |
| Rougher flotation cell volume | 1.4 | m3 | Per cell |
| Total rougher flotation capacity | 22.4 | m3 | Not stated |
| Scavenger flotation cells | 8 | cells | Not stated |
| Scavenger flotation cell volume | 1.4 | m3 | Per cell |
| Total scavenger flotation capacity | 11.2 | m3 | Not stated |
| Conditioning tank volume | 6.5 | m3 | Rougher circuit, PAX and A208 addition |
| ROM tonnage treated (Jan-May 2026) | 12,887 | tonnes | Production record |
| Average throughput (Jan-May 2026) | 85 | tpd | Production record |
| Average mill feed grade (Jan-May 2026) | 26.4 | g/t Au | Production record |
| Average gravity concentrate grade (Jan-May 2026) | 1,572.5 | g/t Au | Production record |
| Overall gold recovery to gravity concentrate (Jan-May 2026) | 70 | wt% Au | Production record |
| Maximum daily gold recovery (Jan-May 2026) | 100 | wt% Au | Production record |
| Minimum daily gold recovery (Jan-May 2026) | 25 | wt% Au | Production record |
| Total plant uptime (Jan-May 2026) | 1,141 | hours | Production record |
| Total plant downtime (Jan-May 2026) | 499 | hours | Production record |
| Total operating time (Jan-May 2026) | 1,640 | hours | Production record |
| Recorded uptime | 70 | % | Production record |
Overview
The Nalunaq processing plant has been designed based on criteria derived from aggregate metallurgical testwork programs completed between project inception in 1992 through 2020 by various project owners. Halyard Engineering of Ontario, Canada built the plant for Amaroq in 2024. The plant has been in startup operation since 2025.
The pilot plant comprises six basic unit operations: crushing, grinding with gravity recovery of gold, flotation, concentrate thickening filtration and bagging, a gold room for smelting of gravity concentrates to doré, and tailings thickening and filtration. The plant is designed to treat nominally 12.5 tph of ROM feed grading between 12.0-20.0 g/t Au and 1.8-3.0 g/t Ag. Ore is fed to the processing plant at a rate of 104,025 tpa or 12.5 tph dry. Processing takes place inside a winterised building. Dust extraction is provided in the crushing plant section only, where the balance of processing is wet and does not require dust extraction.
Key Process Stages
Various sources of ore from the mining operation are blended via stockpiles to provide a consistent feed quality to the process. In the crushing circuit, ore is fed by front-end loader to a 15-tonne live capacity feed hopper fitted with a stationary grizzly with a 250 mm aperture. Oversize material at +150 mm is fed to the jaw crusher, while the grizzly undersize is discharged directly to the jaw crusher product conveyor. Primary crusher discharge is conveyed to a double-deck classifying screen with 35 mm and 19 mm screen apertures. Screen fractions at +35 mm and +19 mm are conveyed to a short-head secondary cone crusher for crushing and recycled back to the classifying screen. Screen undersize at -19 mm is conveyed to the 900-tonne crushed ore stockpile.
The milling circuit is fed via variable speed vibrating feeders located under the crushed ore stockpile, delivering crushed ore to a 330 kW, 2.1 m Ø x 6.1 m EGL primary ball mill. The primary ball mill operates in closed circuit with a 2 mm product classifying screen. Initial gold recovery is by gravity concentrators treating the classifying screen underflow. Gravity concentrator tailings are fed to a classifying cyclone producing flotation feed with a p80 of 75 µm. The nominal capacity of the grinding circuit is 300 tpd of fresh feed at an assumed availability of 95%.
The flotation circuit consists of a single rougher stage with one scavenger stage and three cleaner flotation stages. The rougher circuit is preceded by a 6.5 m3 conditioning tank where PAX and A208 collector reagents are added. Rougher flotation comprises two parallel banks of eight 1.4 m3 flotation cells for a total rougher flotation capacity of 22.4 m3. Rougher flotation tailings gravitates to the scavenger circuit consisting of eight cells each with a capacity of 1.4 m3 for a total capacity of 11.2 m3. Scavenger tailings is treated as final tailings product. The rougher and scavenger flotation concentrates are combined, then fed to a cleaner flotation conditioning tank where further additions of the PAX and A208 collectors are made. Additional MIBC frother is added in the first cleaner flotation circuit. The cleaner flotation circuit comprises three stages of cleaning, where final concentrate is taken from the third cleaner overflow and all other streams are recycled.
Final concentrate at nominally 300 g/t Au and 3-4% As is fed to the concentrate thickener for dewatering to approximately 45% solids, then filtered via horizontal pressure filter to nominally 9% moisture. Planned production of final flotation concentrates ranges between 0.2 and 0.5 dry tpd at a nominal concentrate grade of 300 g/t Au.
Concentrates from the gravity circuit are processed in the Nalunaq gold room. Up to 6 tpd of gravity concentrate can be processed in this section as required. Gravity circuit concentrates at nominally 3,890 g/t Au and 581 g/t Ag are fed to the gravity tables for upgrading, producing final concentrates which are then combined with silica, borax, and sodium nitrate fluxes and batched in typically 27 kg lots for smelting by induction furnace once every two days to produce a doré gold product for onward sale.
Additional Interesting Data and Summary
Production records for Nalunaq pilot plant processing operations spanning the period 1 January 2026 to 31 May 2026 were provided by the Nalunaq metallurgical team to the QP for review. The total ROM tonnage treated over the period was 12,887 tonnes, processed at an average throughput of 85 tpd. Average mill feed grade over the period was reported as 26.4 g/t Au. The associated average grade of gravity concentrate produced was 1,572.5 g/t Au for overall recovery of gold to the gravity concentrate of 70 wt% Au, with a maximum daily gold recovery of 100 wt% and a minimum daily gold recovery of 25 wt% recorded over the period.
Total plant recorded uptime over the period was 1,141 hours with a downtime of 499 hours, from a total operating time of 1,640 hours, indicating an uptime of 70% achieved over the period. Plant operating time as reviewed appears to be somewhat below design. Gold concentrate grades achieved over the period appear to be on target. Comparison of an overall metallurgical recovery of 70 wt% Au as achieved over the period to the design criterion of 94 wt% Au recovery suggests that substantial process optimisation to meet gold concentrate grades and recoveries targeted in production operations is achievable going forwards.
Key Processes
- Crushing: jaw crusher with secondary cone crusher in closed circuit with a double-deck screen
- Grinding: primary ball mill in closed circuit with a 2 mm screen
- Gravity recovery: concentrators treating screen underflow
- Flotation: rougher, scavenger, and three cleaner stages with PAX and A208 collectors
- Dewatering: concentrate thickener and horizontal pressure filter
- Gold room: gravity tables, flux addition, and induction furnace smelting to doré
- Tailings: thickening and filtration
Source: NI 43-101 Technical Report – Mineral Resource Estimate (MRE5) for the Nalunaq Gold Mine, Greenland, 27 June 2026. Project website: Nalunaq Gold Mine
Consolidated report summaries
The following former standalone pages about this operation were consolidated here on October 25, 2026. They are retained for source traceability; dates and figures reflect each report’s own effective date and may be superseded by the current information above.
Nalunaq — 2022 NI 43-101 Technical Report
Nalunaq — 2022 NI 43-101 Technical Report
| Company | Nalunaq A/S |
| Date | 2022 |
| Region | Greenland |
| Commodities | Gold |
Executive Summary
SRK Consulting prepared this NI 43-101 Technical Report for Nalunaq A/S in October 2022. The report outlines recovery methods commissioned from Halyard Inc to investigate future processing and recovery requirements. The plant has not been commissioned, and a detailed report is not available, so the information is summarized for information purposes.
Amaroq currently plans mined material would be fed to the processing facility at a base rate of 104,025 t per year at a nominal feed rate of 300 t per day for 365 days in the year. The processing facility will consist of crushing, grinding, gravity recovery, flotation, thickening, tailings filtering, and a gravity concentrate smelting facility.
The current flowsheet is developed around the high propensity of the gold at Nalunaq to be recovered in a gravity concentration circuit, calculated to be in the order of 65-75%. An additional 20-25% of the gold in the remaining slurry will be recovered by the flotation circuit downstream of the gravity concentration circuit.
Reports
- entities/Nalunaq_Mine
Website: https://www.amaroqminerals.com/projects/nalunaq/
Report Date: 2022
Region: Greenland
Project Status:
Commodity: Gold
Throughput:
Mine Life:
Mine Type:
Ore type:
