

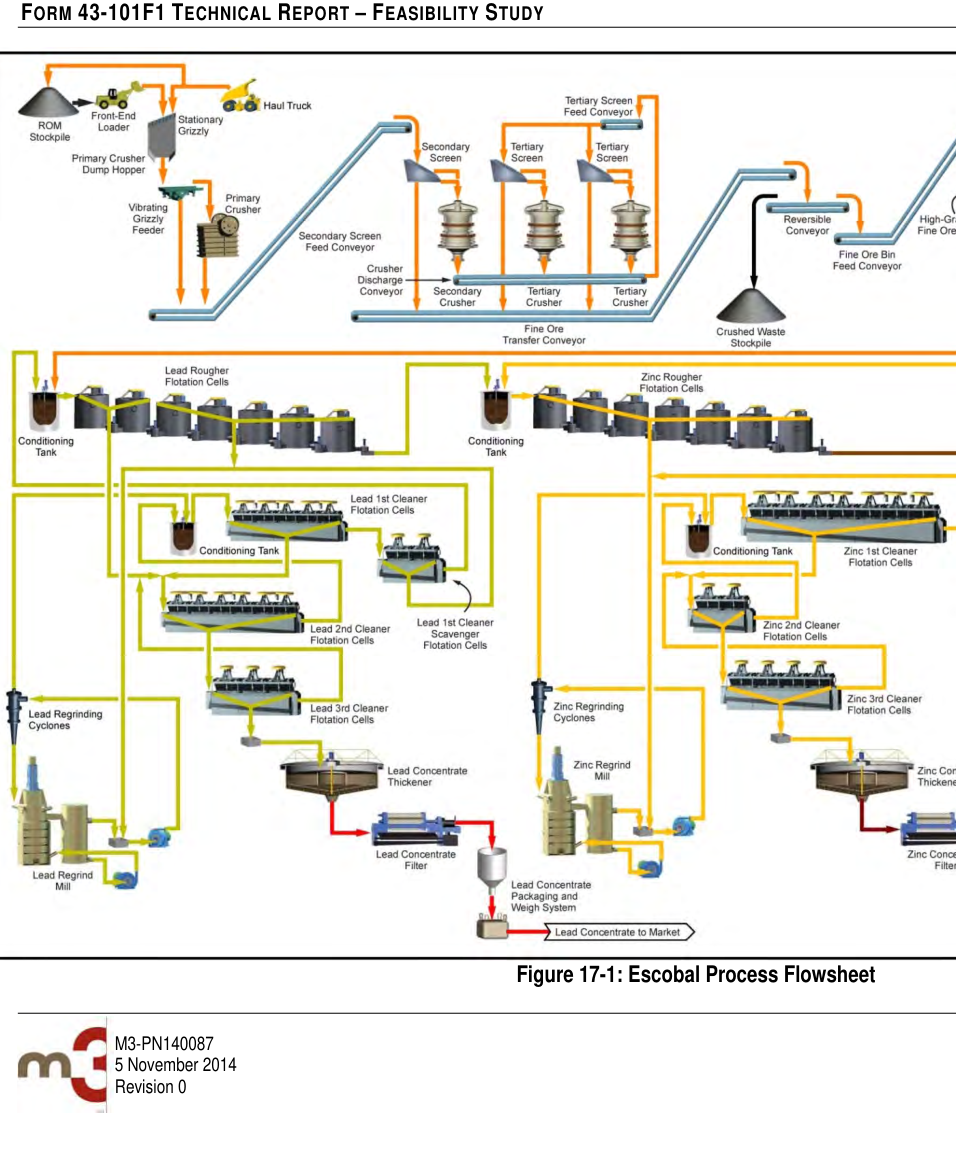
Tahoe Resources' 2014 feasibility study for the Escobal mine describes a three-stage crushing, single ball mill and differential flotation plant built for 3,500 t/d and sized for 4,500 t/d, with filtered tailings dry stacked or sent underground as paste.
The Escobal mine lies in southeast Guatemala, about 40 km east-southeast of Guatemala City and 3 km east of San Rafael Las Flores in the Department of Santa Rosa. In 2014 Tahoe Resources Inc. owned and operated it through its wholly owned subsidiary Minera San Rafael, having bought the deposit from Goldcorp in 2010. The feasibility study by M3, dated November 5, 2014, covers an operating underground longhole stoping mine in an intermediate-sulphidation silver-gold-lead-zinc vein deposit. The mill produced its first concentrate on September 30, 2013, and commercial production was declared in January 2014. The mill was running at its 3,500 t/d design rate and preparing to expand to 4,500 t/d. Proven and probable reserves were 31.4 Mt at 347 g/t silver, containing 350.5 million ounces.
Critical Data
| Parameter | Value | Unit | Notes |
|---|---|---|---|
| Design throughput | 3,500 | t/d | 1.28 Mt per year |
| Expansion throughput | 4,500 | t/d | Main equipment already sized for it |
| June 2014 average throughput | 3,708 | t/d | During ramp-up |
| Crushed product size | 9 | mm | 80% passing, three-stage crushing |
| Ball mill motor | 3,357 | kW | Fixed speed synchronous |
| Ball mill design rate | 203.8 | t/h | Solids |
| Grind size | 105 | µm P80 | Flotation feed |
| Lead regrind product | 37 | µm P80 | Eirich vertical mill |
| Mill feed silver grade | 581 | g/t | Life of mine to June 2014 |
| Silver recovery | 86.2 | % | Total, both concentrates |
| Lead concentrate grade | 44.7 | % Pb | 23,959 g/t silver |
| Zinc concentrate grade | 51.9 | % Zn | Life of mine to June 2014 |
| Tailings filter cake moisture | About 14 | % | Three Diemme GHT 2000 filters |
| Expansion capital, process plant | 13.2 | US$ million | Mostly a new tailings filter |
Overview
Escobal uses conventional differential flotation. Ore is crushed in three stages to 9 mm and ground in a single ball mill to 105 µm. A lead circuit then floats a silver-rich lead concentrate that carries most of the gold, while zinc is depressed. The lead tailings go to a zinc circuit where sphalerite is reactivated and floated into a zinc concentrate with minor precious metals. Both concentrates are thickened, pressure filtered and packed in one or two tonne bags inside 20 t shipping containers for export. Flotation tailings are thickened and filtered, then conveyed either to a dry stack facility or to the paste backfill plant. Process water is recycled as far as possible to limit treatment and discharge.
The flowsheet came from flotation test work and pilot plant studies run between 2009 and 2013.
Key Process Stages
Primary crushing
A front-end loader feeds ore from a stockpile into the crusher hopper. A stationary grizzly holds back rocks over 600 mm for a Tramac hydraulic breaker. A Telsmith vibrating grizzly feeder sends ore finer than 100 mm around the crusher. Oversize goes to a Telsmith 3055 single-toggle jaw crusher with a 160 kW motor, which crushes to 80% passing 150 mm at a nominal 219 dmt/h.
Secondary and tertiary crushing
A triple deck Telsmith screen feeds a 225 kW secondary cone crusher and passes fines below 10 mm straight to the fine ore conveyor. Crusher product joins the discharge from two tertiary cone crushers and returns on a common conveyor to two triple deck tertiary screens. These screens choke feed the tertiary crushers and pass the final product at 80% minus 9 mm. Six 914 mm conveyors move the ore, and two 2,000 t fine ore bins hold it ahead of the mill.
Grinding
Belt feeders under the bins fill the ball mill feed conveyor. Zinc cyanide and zinc sulphate go into the mill feed chute. The ball mill runs at 70% solids with up to 30% ball charge, fed by a ball feeder of up to 15 t/d. Its 3,357 kW motor and 203.8 t/h design rate already cover the 4,500 t/d case, which needs only a larger pinion gear that the company already held in stock. A trommel returns oversize to the crushing plant, and four Krebs gMax26 cyclones, three running, classify the slurry to 105 µm.
Lead flotation
Cyclone overflow at about 30% solids is conditioned and floated at about pH 8 in seven 40 m3 Wemco self-aspirated rougher cells. Rougher concentrate is reground in an Eirich ETM300 vertical mill with Krebs cyclones from 100 µm to 37 µm. Cleaning runs in three stages of Westpro cells: five 5 m3 first cleaners with two cleaner scavengers, four 5 m3 second cleaners in two banks, and three 1.5 m3 third cleaners. The final lead concentrate leaves the third cleaner at about 6.7 t/h. Reagents include potassium amyl xanthate, Flomin C-7931 promoter, MIBC frother, and zinc cyanide and zinc sulphate to depress pyrite and sphalerite.
Zinc flotation
Lead rougher tailings enter a 39 m3 conditioning tank with activator, collector and promoter, then seven more 40 m3 Wemco rougher cells. Zinc rougher concentrate is reground with a 300 kW mill and cyclones and cleaned in a circuit that follows the lead circuit's layout.
Dewatering and tailings
Concentrate thickeners raise each product to about 65% solids. Three Diemme GHT1200 pressure filters, one for lead, one for zinc and one standby, produce the filter cake for bagging. A 16 m WesTech high rate thickener takes the tailings from about 25% to 60% solids. Three Diemme GHT 2000 filters, each rated at 85 wet t/h, produce cake at about 14% moisture, and a reversing conveyor sends it to the dry stack radial stacker or to the paste plant.
Additional Interesting Data and Summary
To the end of June 2014 the mill had treated 743,996 t and produced 14,804 t of lead concentrate and 14,053 t of zinc concentrate. These held about 12 million ounces of silver. Total recoveries over that period, including start-up and ramp-up, were 86.2% for silver, 67.4% for gold, 90.5% for lead and 89.4% for zinc. In the second quarter of 2014, silver and lead recovery to the lead concentrate ran 2.5% and 8% above the test work figures. Gold recovery to lead concentrate and zinc recovery to zinc concentrate came in below them.
The plant expansion budget of about US$13.2 million is dominated by a Micronics LASTA pressure filter, able to treat 2,000 dry t/d at 90% availability, which accounts for about US$8.8 million. The new filter fits in the existing tailings filtration building.
The study projected average production of 19.1 million ounces of silver a year over the first ten years.
Key Processes
- Rock breaking and jaw crushing to 150 mm
- Secondary and tertiary cone crushing to 9 mm with triple deck screens
- Ball milling with cyclones to 105 µm
- Lead rougher flotation, vertical mill regrinding and three-stage cleaning
- Zinc activation, rougher flotation, regrinding and cleaning
- Concentrate thickening, pressure filtration and bagging
- Tailings thickening and pressure filtration for dry stacking and paste backfill
Source: Escobal Mine Guatemala, NI 43-101 Feasibility Study, November 5, 2014.
Project website: Escobal Mine
